
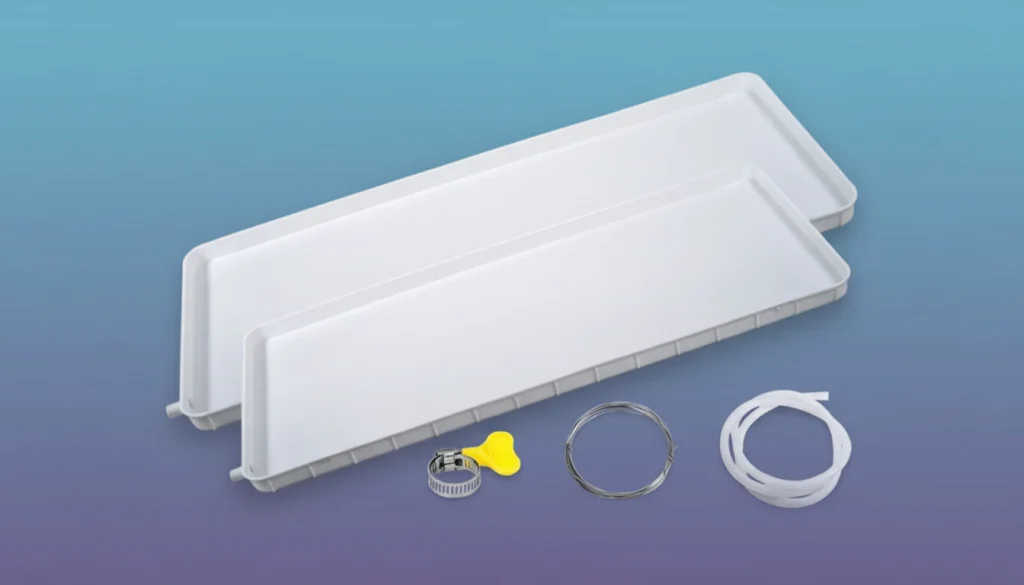
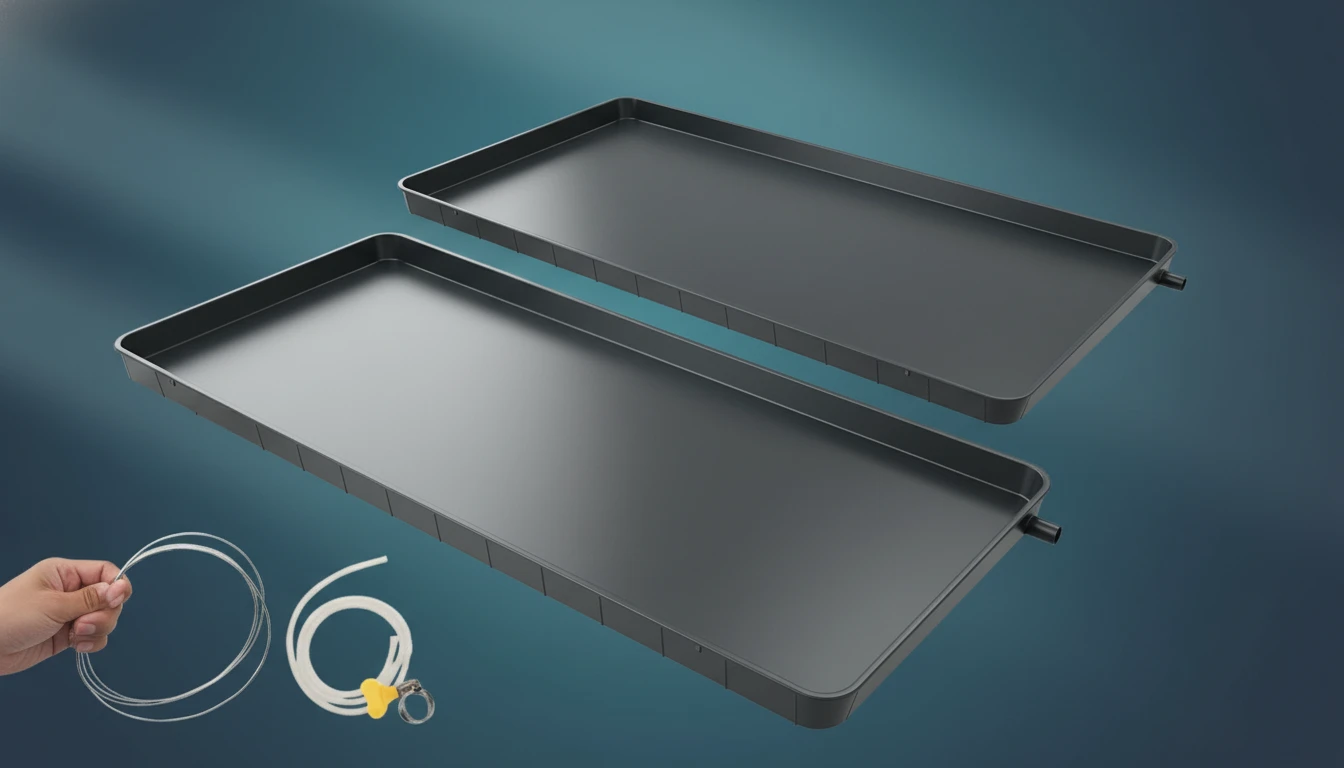
– Monolithic Integrity: Single-shot injection molding creates a continuous part with zero seams, welds, or glue joints, eliminating the primary failure points of traditional pans.
– Integrated Slope: The draft and drainage pitch are machined directly into the mold steel, guaranteeing positive drainage and preventing stagnant water accumulation.
– Corrosion Immunity: Switching to thermoplastics (like PP or ABS) permanently solves the rusting issues inherent in galvanized steel pans.
– Structural Ribbing: Advanced mold design incorporates honeycomb or grid ribbing to support water weight without the warping that causes overflow leaks.
Why Are Traditional Condensate Pans Failing?
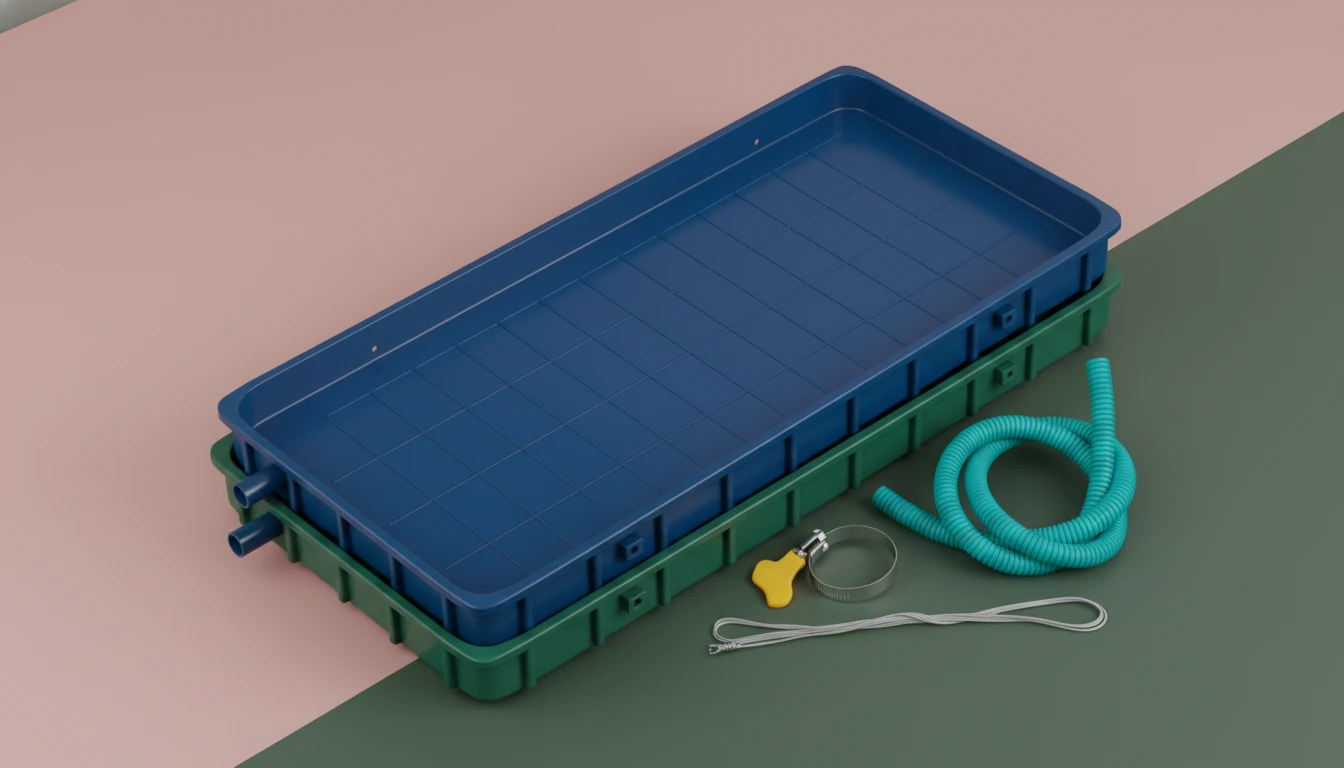
In my years managing HVAC production lines, the single most common warranty claim—and the most damaging to a building owner—was the condensate leak.
Traditionally, pans were made from galvanized sheet metal (welded at corners) or vacuum-formed plastic. Both have fatal flaws. Metal eventually rusts due to the acidic nature of condensate and chemical cleaners. Vacuum forming yields thin corners and requires secondary gluing for drain ports.
The industry solution is single shot injection molding. By injecting the entire HVAC condensate pan—floor, walls, mounting brackets, and drain bosses—in one cycle, we create a leak-proof HVAC design that is structurally superior and chemically inert.
Key Parameters: Fabricated vs. Molded Pans
To achieve HVAC maintenance reduction, we must compare the physical properties of the "old way" versus the seamless molded approach.
| Parameter | Fabricated Metal / Vacuum Form | Single-Shot Injection Molded | Production Benefit |
|---|---|---|---|
| Leak Paths | High (Welds, folded corners, glued fittings) | Zero (Monolithic structure) | Eliminates field failure liability. |
| Drainage Slope | Variable (Depends on installation/bending) | Fixed (Machined into mold) | Guarantees gravity drainage; no "ponding." |
| Corrosion Resistance | Low (Zinc coating wears off) | Total (Polymer is inert) | Rust-free drain pans last the life of the unit. |
| Detail Integration | Low (Requires secondary assembly) | High (Clips/bosses molded in) | Reduces assembly line labor and SKU count. |
Step-by-Step: Engineering the Perfect Pan
Designing a large surface-area part like a drain pan requires mastering flow and shrinkage. Here is the process we use to ensure the pan comes out of the mold flat and watertight.
1. Material Selection (Chemical & Fire Resistance)
We typically use Polypropylene (PP) with 20% Talc filler or كيف تختبر التسريبات في الإنتاج الضخم؟.
- Why: Unfilled PP shrinks too much (approx. 1.5-2.0%), causing the pan to warp and lose its drainage slope. Talc reduces shrinkage to ~1.0% and increases stiffness. The material must also pass UL 94 (5VA or V-0) flammability tests.
2. The "Single Shot" Strategy
We utilize a high-tonnage press (usually 800T to 1500T). The mold is designed with a Hot Runner System.
- Factory Reality: We use multiple valve gates to fill the large area quickly. However, we must sequence them to push the "weld lines" to areas that do not hold water, or ensure the melt temperature is high enough that the knit lines fuse completely.
3. Integrated Slope Design
The most critical feature of a drain pan is the "pitch." In a single shot injection molding tool, we cut the mold cavity on a bias.
- The Math: We aim for a minimum 1/4 inch per foot slope towards the drain boss. Because this is hard-tooled, every single part produced has the exact same perfect drainage slope.
4. The Drain Boss
Instead of gluing in a PVC fitting later, we use a threaded core pull in the mold. The press opens, the core unscrews, and the part ejects with perfectly formed internal threads (NPT or BSP). This eliminates the leak path between the fitting and the pan.
While steel has higher tensile strength, a properly designed injection molded pan uses structural ribbing (honeycomb or cross-hatch) to achieve superior rigidity-to-weight ratio. Furthermore, plastic absorbs vibration better than metal, reducing noise without fatiguing or cracking over time.
By molding the threaded drain boss as an integral part of the pan (using an unscrewing mold core), there is no seam, glue, or gasket between the port and the pan body. This monolithic design removes the most common leakage point in HVAC condensate systems.
Advantages and Disadvantages
| Feature | Advantages | Disadvantages |
|---|---|---|
| Monolithic Geometry | No seams to leak; rust-free drain pans. | High initial tooling cost ($50k – $150k for large molds). |
| Integrated Features | Sensor mounts and float switch clips molded directly in. | Difficult to modify design once steel is cut. |
| Surface Finish | Smooth surface prevents sludge/algae adhesion. | Large flat surfaces are prone to sink marks if ribs are too thick. |
Practical Tips for Molded Pan Production
-
Watch the Wall Thickness:
In HVAC condensate pan design, consistent wall thickness is vital. If the bottom of the pan is 3mm but the corners are 5mm, the corners will cool slower, causing internal stress. This stress pulls the corners up (warpage), which can reverse the drainage slope. We use coring-out techniques to keep walls uniform. -
Antimicrobial Additives:
We often blend antimicrobial agents directly into the hopper during molding. This prevents the growth of mold and slime (biofilm) on the pan surface, a key selling point for HVAC maintenance reduction. Unlike spray-on coatings, this protection is molecular and never washes off. -
Secondary Drain Safety:
Always design the mold with a "secondary" or "auxiliary" drain port boss, slightly higher than the primary. Even if the customer doesn’t use it, having the molded-in boss ready for knockout allows the unit to meet building codes without needing a different pan SKU.
HVAC Application Scenarios
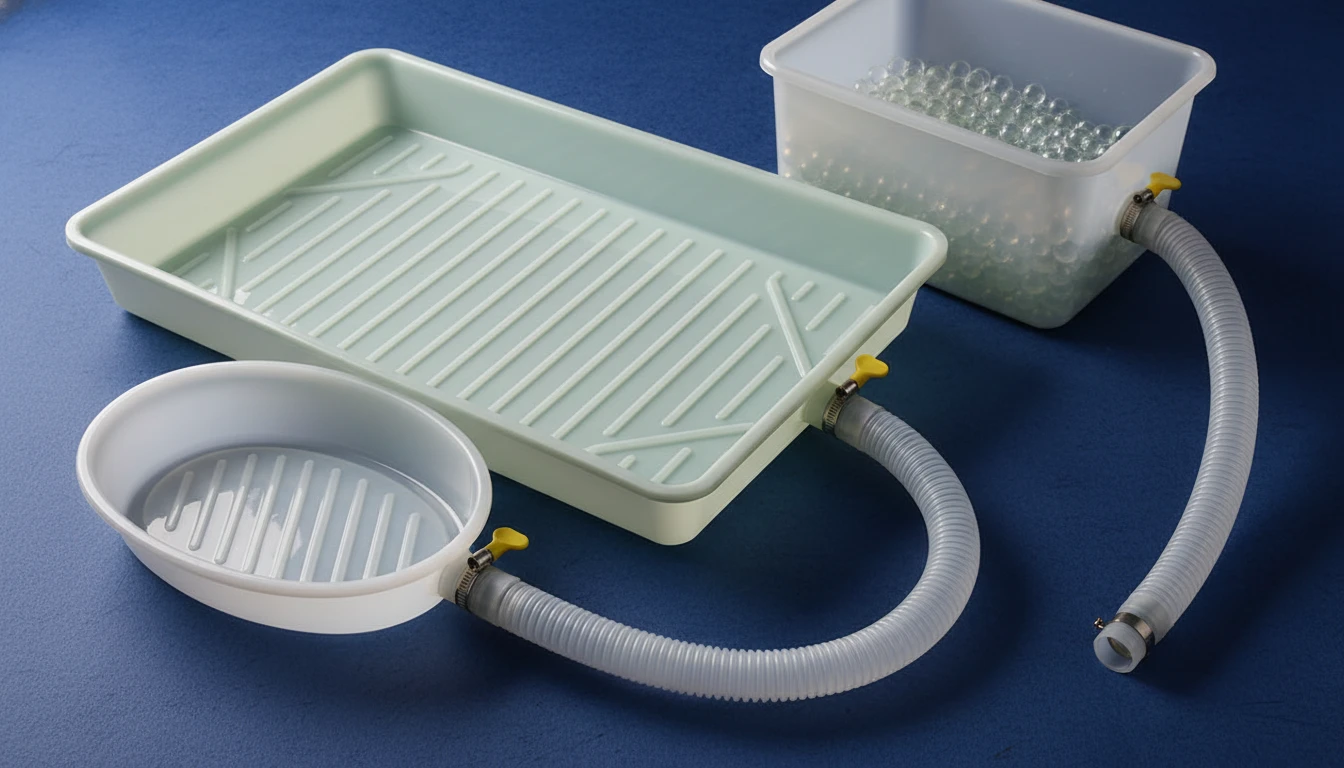
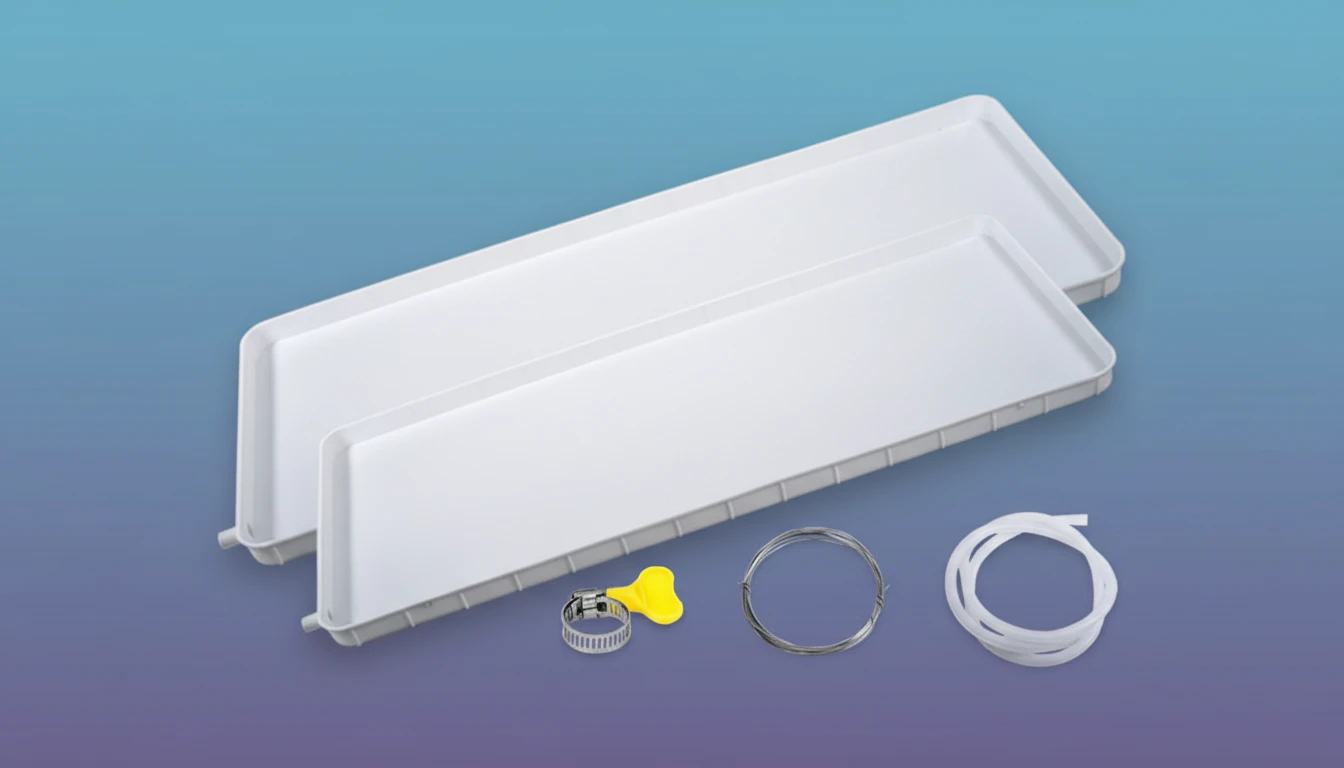
- Ductless Mini-Splits: Long, narrow pans that require high precision to fit inside compact wall units. Injection molding allows for complex geometry to route around the fan motor.
- Commercial Roof Top Units (RTUs): Large pans (4ft x 4ft). We mold these in sections with "labyrinth seals" or, for smaller RTUs, as one massive single shot using a 2000-ton press.
- Fan Coil Units (FCU): Vertical stack units where the pan must act as a structural base for the coil. Glass-filled polypropylene is used here for load-bearing capacity.
This is a misconception based on cheap plastics. Engineered HVAC resins like Glass-Filled Polypropylene or Polycarbonate blends have Heat Deflection Temperatures (HDT) well above 200°F (93°C), easily withstanding the ambient heat from furnaces or electric strip heaters located near the coil.
Because injection molds are CNC machined to exact tolerances, the floor of the pan can be engineered with flow channels and a guaranteed positive slope. Vacuum forming or metal bending often result in 'low spots' where water pools, leading to bacterial growth.
FAQ: Troubleshooting Molded Pans
Can injection molded pans crack during shipping?
If the material is too brittle (like cheap Polystyrene) or if it’s extremely cold, yes. This is why we prefer Copolymer Polypropylene, which has excellent impact resistance even at sub-zero temperatures, ensuring the pan arrives at the job site intact.
How do you test for leaks in mass production?
حسّن كفاءة أنظمة التكييف والتهوية باستخدام حلول أوركا كور التقنية.
Are these pans compatible with condensate pumps?
Yes. We often design specific "landing pads" or clip-on features within the mold geometry to accept standard condensate pumps, keeping them off the bottom of the pan to reduce vibration noise.
What happens if the drain threads strip?
Since the threads are plastic, over-tightening a metal fitting can strip them. We recommend using PVC fittings or designing the mold to accept a sonic-welded brass insert for heavy-duty commercial applications.
Is UV resistance required?
For indoor units, no. But for outdoor condensing units or RTUs, the plastic must have UV stabilizers added. Without it, the sun will chalk the plastic and cause micro-cracking, eventually leading to a leak.
Technical Summary
The shift to single shot injection molding for HVAC condensate pans represents a definitive upgrade in system reliability. By replacing multi-piece assemblies with a single, monolithic thermoplastic component, manufacturers eliminate the chemical vulnerability of metal and the mechanical vulnerability of glued joints. Through precise mold engineering—incorporating fixed drainage slopes, structural ribbing, and integrated thread bosses—we achieve a leak-proof HVAC design that significantly contributes to HVAC maintenance reduction and long-term homeowner satisfaction.





