
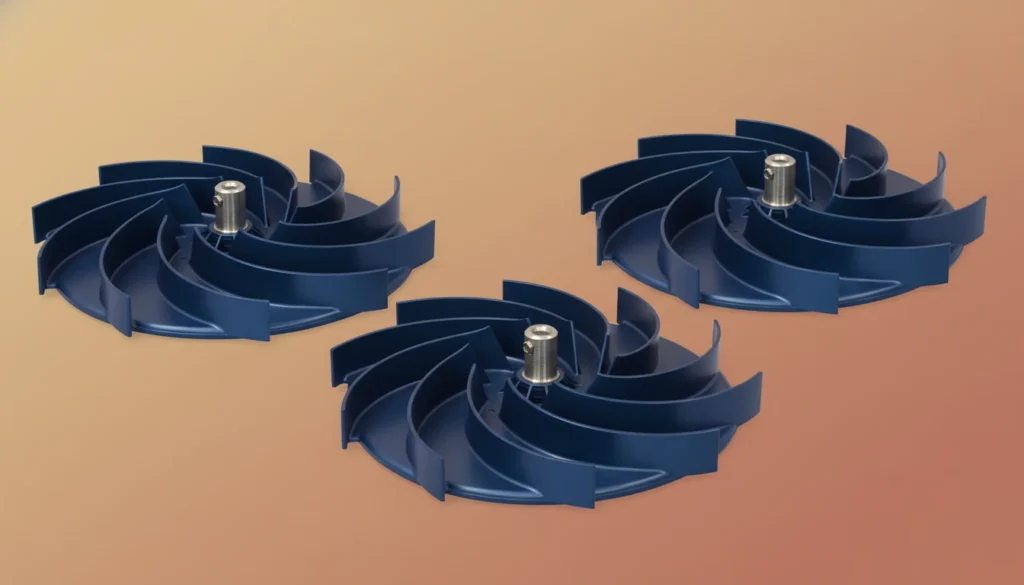
– Overmolding Thermoplastic Elastomers (TPE) onto rigid substrates significantly reduces Noise, Vibration, and Harshness (NVH) in HVAC systems.
– Chemical bonding between the substrate and TPE eliminates the need for manual assembly of rubber grommets or seals.
– Selecting the correct Shore A hardness and compression set values is critical for effective vibration isolation.
– Utilizing overmolding strategies lowers total manufacturing costs by consolidating parts and reducing assembly cycle time.
What Is the Role of Overmolding in NVH Reduction?
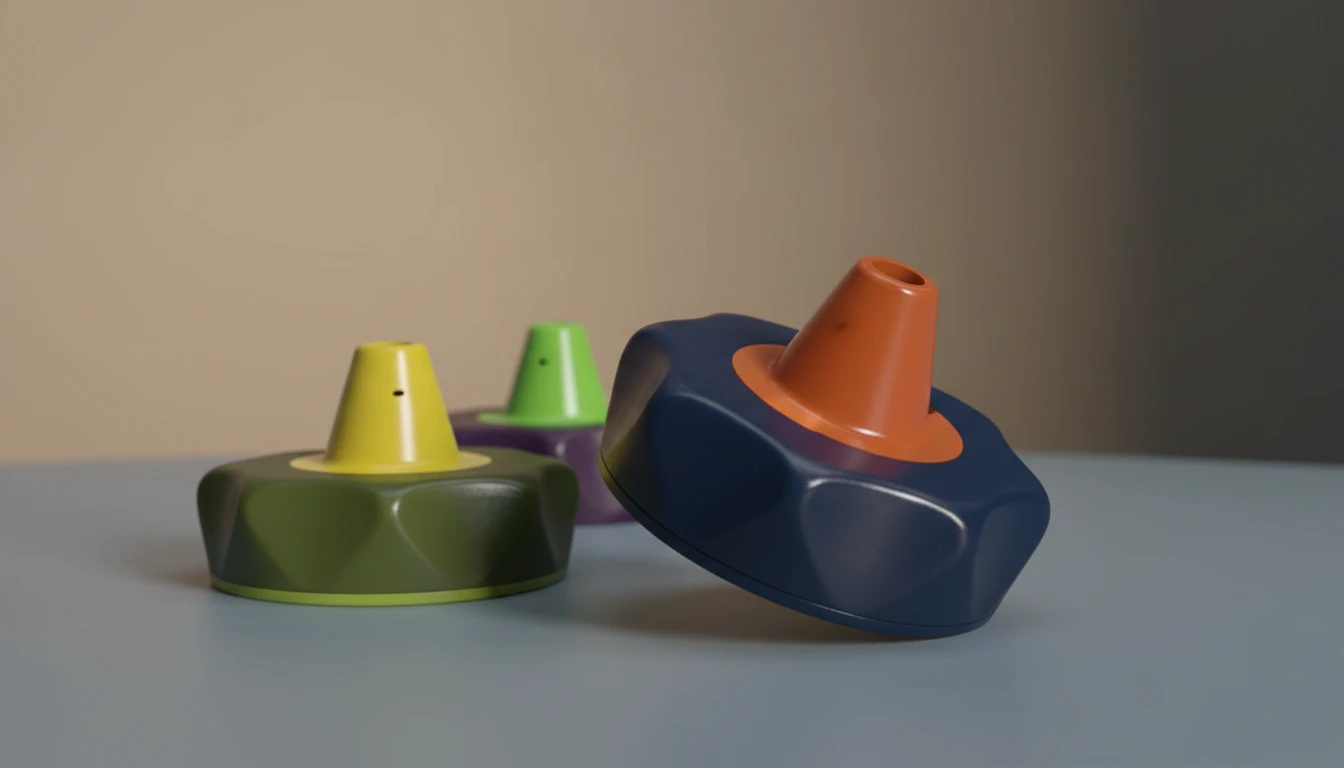
Overmolding is an injection molding process where a secondary material, typically a soft Thermoplastic Elastomer (TPE) or Thermoplastic Vulcanizate (TPV), is molded over a rigid substrate material like Polypropylene (PP) or Acrylonitrile Butadiene Styrene (ABS). In the context of Heating, Ventilation, and Air Conditioning (HVAC), this process is engineered specifically for NVH reduction (Noise, Vibration, and Harshness).
By integrating vibration dampening plastics1 directly into the structural component, manufacturers create a monolithic part that absorbs kinetic energy. This approach replaces traditional methods of installing separate rubber grommets, foam tapes, or mechanical fasteners, which often loosen over time and contribute to rattles. This strategy is essential for achieving quiet HVAC design requirements in residential and automotive applications.
Materials with low compression set resist permanent deformation under load, maintaining the elastic gap necessary to absorb vibration over the product's life.
While harder materials reflect sound, softer TPEs (Shore 30A-60A) are generally required to decouple vibrating components and absorb resonance frequencies effectively.
What Are the Critical Parameters for HVAC Overmolding?
To ensure successful overmolding HVAC parts, specific material properties must be controlled. The interaction between the rigid substrate and the soft overmold defines the dampening capability.
| Parameter | Unit / Standard | Recommended Range | Technical Note |
|---|---|---|---|
| Shore Hardness | Shore A (ASTM D2240) | 30A – 70A | Softer grades offer better isolation; harder grades offer structural support. |
| Compression Set | % (ASTM D395) | < 35% @ 70°C | Low compression set prevents the dampener from flattening out over time. |
| Bond Strength | MPa (ISO 11339) | > 2.5 MPa | Critical to prevent delamination during high-frequency vibration2. |
| Service Temperature | °C | -40°C to 125°C | Must withstand compressor heat and outdoor freezing conditions. |
| Damping Factor (Tan Delta) | Dimensionless | > 0.1 | Higher Tan Delta indicates better energy absorption capabilities. |
How Is the TPE Overmolding Process Executed Step-by-Step?
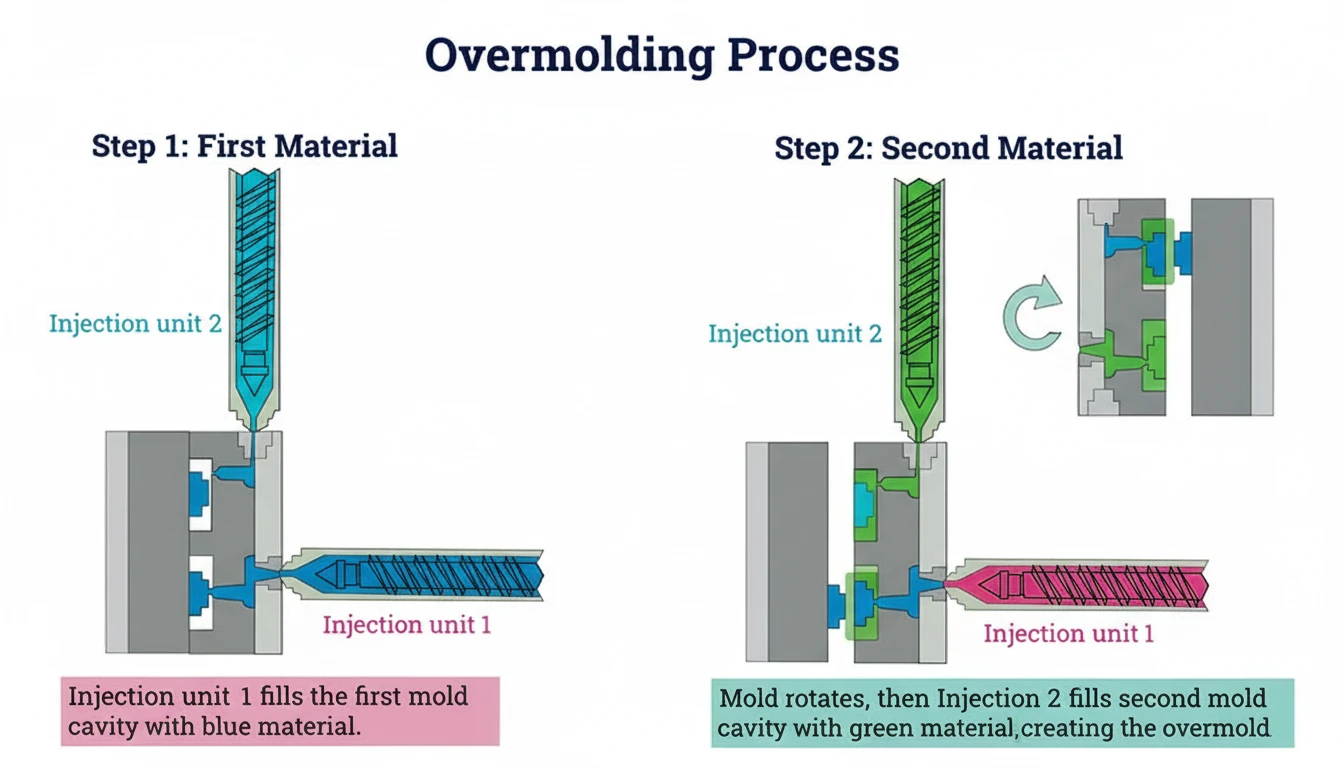
The TPE overmolding process for vibration dampening involves a precise multi-shot sequence.
- Substrate Injection: 2. Come si confronta l'overmolding con l'uso di guarnizioni in gomma separate in termini di costo?.
- Mold Transfer/Rotation: The mold core rotates, or the part is robotically transferred to a second cavity. The substrate retains residual heat, which aids in chemical bonding.
- Overmold Injection: The TPE is injected into the second cavity, flowing over specific areas of the substrate (mounting points, seal interfaces).
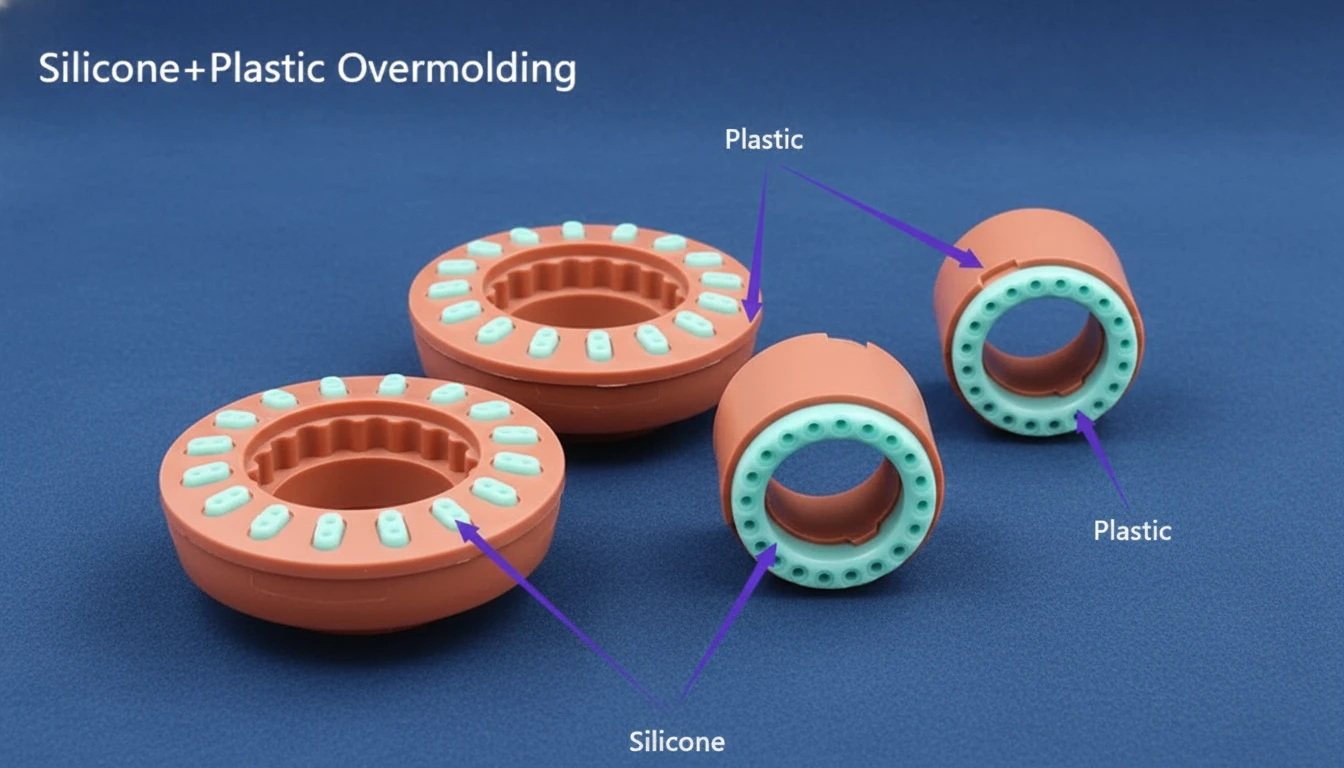
- Bonding and Cooling: The TPE chemically bonds to the substrate while cooling. Mechanical interlocks (holes or undercuts in the substrate) are filled to reinforce the connection.
- Ejection: The finished multi-material part is ejected as a single unit, ready for installation without secondary assembly.
What Are the Advantages and Disadvantages of This Strategy?
Implementing overmolding for quiet HVAC design offers significant benefits but introduces specific manufacturing complexities.
| Feature | Advantages | Disadvantages |
|---|---|---|
| NVH Performance | Superior vibration isolation due to seamless integration; eliminates gaps where rattles occur. | Requires precise material science to match vibration frequencies; incorrect hardness can amplify noise. |
| Assembly | Eliminates manual installation of O-rings, gaskets, and grommets; reduces labor costs. | High initial tooling investment (two-shot molds or rotary platens are expensive). |
| Durability | Chemical bond prevents seals from shifting or falling out during operation. | If the bond fails, the entire component is scrap; repair is not possible. |
| Design Freedom | Allows for complex dampening geometries not possible with extruded rubber. | Material compatibility is restrictive; TPE must be chemically compatible with the substrate. |
What Practical Insights Can Optimize Vibration Dampening?
Based on extensive factory floor experience, the following insights are crucial for high-performance NVH reduction:
- Mechanical Interlocks are Mandatory: While chemical bonding is effective, the high-frequency vibration in HVAC compressors can fatigue the chemical bond. Always design "through-holes" or dovetail undercuts in the rigid substrate to physically lock the TPE in place.
- Gate Location Matters: Avoid gating the TPE directly onto a thin section of the substrate. The shear heat and pressure can wash out (melt/deform) the rigid part. Gate in a thick section and flow toward thin seal areas.
- Wall Thickness Ratios: To prevent sink marks and warpage in the rigid part, ensure the TPE wall thickness does not exceed the substrate thickness significantly. A ratio of 1:1 or less is ideal.
- Material Compatibility: For Polyamide (PA/Nylon) substrates, standard TPEs often fail to bond. Use modified TPEs specifically formulated for adhesion to polar engineering plastics.
Elevating the substrate surface temperature promotes molecular entanglement between the rigid plastic and the molten TPE, significantly enhancing adhesion.
Relying solely on chemical bonds is risky for dynamic loads; mechanical interlocks must be added to prevent catastrophic delamination during high-cycle vibration.
Where Are These Overmolding Strategies Applied?
- Compressor Mounting Feet: Overmolding heavy-duty TPV onto steel or rigid plastic inserts to isolate compressor vibration from the chassis.
- Blower Fan Housings: Overmolding HVAC parts like fan shrouds with soft TPE edges to decouple the fan from the metal ductwork.
- Air Diverter Doors: Soft TPE seals overmolded onto HVAC flap doors to ensure silent closure and prevent air leakage (whistling noises).
- Condensate Drain Pans: Integrated TPE seals to prevent rattling against the frame and ensure watertight performance.
What Are the Recommended Process Adjustments?
To maximize vibration dampening plastics performance, adhere to these processing guidelines:
- Shot sequencing: Ensure the substrate is clean and warm (if insert molding) or molded immediately prior (if multi-shot) to maximize adhesion.
- Injection Speed: Use a medium-to-fast injection speed for the TPE to prevent premature freezing, which compromises the bond, but avoid shear burning.
- Pack and Hold: TPEs are spongy; adequate hold pressure is required to minimize shrinkage, but excessive pressure can induce residual stress that affects dampening frequency.
Frequently Asked Questions (FAQ)
1. Which TPE material is best for high-temperature HVAC compressors?
For high-temperature environments (continuous use >100°C), Thermoplastic Vulcanizate (TPV) is recommended over standard Styrenic Block Copolymers (TPS) due to its superior heat resistance and compression set properties.
2. How does overmolding compare to using separate rubber grommets for cost?
Riduci il Rumore HVAC con le Tecniche di Sovrastampaggio TPE.
3. Can I overmold TPE onto metal HVAC components?
Yes. This is technically "insert molding3." The metal must be primed or physically prepared (degreased, sandblasted, or coated with adhesive) to ensure a strong bond, as TPE does not naturally chemically bond to metal.
4. How do I determine the right shore hardness for vibration dampening?
This depends on the frequency of the vibration. Lower frequencies generally require softer materials (Shore 30A-50A) to absorb energy, while higher load-bearing applications may require Shore 60A-80A. Finite Element Analysis (FEA) is recommended.
5. What is the biggest cause of delamination in overmolded HVAC parts?
The most common cause is material incompatibility (e.g., trying to bond TPE to Polypropylene without matching polarity) or a cold substrate surface that prevents molecular diffusion at the interface.
Summary
Effective NVH reduction in modern HVAC systems relies heavily on advanced overmolding strategies. By integrating TPE overmolding with rigid substrates, manufacturers can produce components that offer superior vibration isolation, airtight sealing, and long-term durability. While the initial investment in mold design and material selection is higher, the result is a cost-effective, quiet HVAC design4 that meets the stringent demands of today’s market. Prioritizing mechanical interlocks and verifying chemical compatibility are the cornerstones of success in this process.
-
Explore the science behind vibration dampening plastics to improve HVAC efficiency and comfort. ↩
-
Understanding high-frequency vibration can help you design more durable HVAC systems. ↩
-
Insert molding techniques can enhance product performance; learn how to implement them effectively. ↩
-
Discover strategies for creating quieter HVAC systems that enhance user experience and satisfaction. ↩





