
- Chinese injection molding manufacturers typically offer 40–60% lower tooling costs than equivalent European or North American suppliers.
- ISO 9001 certification, dedicated quality control staff, and English-language project management are the three non-negotiables when qualifying an HVAC plastic parts manufacturer in China.
- Lead time from approved design to first-article delivery is typically 6–10 weeks for new tooling; production runs deliver in 3–5 weeks.
- The biggest sourcing mistake is treating HVAC plastic parts as commodities — the right manufacturer understands UL 94 flame ratings, UV weathering, and HVAC-specific tolerances.
- HVACore has supplied injection-molded HVAC components to OEMs in North America, Europe, and Australia for over a decade, with all production held to ISO 9001 and UL 94 standards.
Why HVAC Buyers Source Plastic Components from China
A procurement director at a mid-size HVAC OEM put it bluntly: “We tried domestic tooling for two years. The quality was fine but we couldn’t compete on price.” His company switched to a Chinese manufacturer, cut tooling cost by 52%, and kept the same first-pass yield. That story repeats itself across the HVAC industry every year.
China accounts for over 60% of global injection-molded plastic component production. For HVAC specifically, the country’s manufacturing base offers mature supply chains for ABS, ASA, PP, and PC/ABS — the core material set for vents, ductwork, filter frames1, brackets, and electrical enclosures. Labor costs, tooling infrastructure, and supply chain density combine to deliver cost structures that domestic alternatives cannot match at scale.
The risk is real, though. Not every Chinese manufacturer understands HVAC-specific requirements: UL 94 flame ratings for plenum applications, ASA weathering performance for outdoor units, or the dimensional stability demands of snap-fit filter frames. The selection process matters as much as the decision to source internationally.
How to Qualify an HVAC Plastic Parts Manufacturer in China
Qualification starts with three non-negotiables: ISO 90012 certification (documents that processes are controlled and repeatable), English-language project management (critical for RFQ, DFM, and inspection communication), and a dedicated quality team with documented inspection protocols for dimensional checks, material certification, and first-article approval.
Beyond these, look for HVAC-specific experience. A manufacturer that has produced air vents3, damper housings, or filter frames understands draft angles for snap-fit features, the surface texture requirements for visible grille faces, and the wall thickness tolerances needed for consistent assembly. Ask to see sample parts and documented PPAP or FAI reports from similar programs.
Factory audit is strongly recommended for new supplier qualification. Key items to verify in person: injection molding machine tonnage range and condition, mold room capability (in-house vs. outsourced), material traceability documentation, and QC laboratory equipment (CMM, hardness tester, colorimeter). A 30-minute factory walkthrough eliminates more risk than 10 rounds of email.
| Criteria | Minimum Standard | Why It Matters |
|---|---|---|
| Quality certification | ISO 9001:2015 | Documented process control and audit trail |
| Machine range | 60–1,500 ton | Covers small brackets to large plenum housings |
| Material traceability | Lot certificates retained ≥2 years | Required for UL 94 compliance claims |
| English PM contact | Dedicated, not shared | Prevents specification errors and delays |
| DFM capability | Written DFM report before tooling | Reduces first-article failures by 60–80% |
| HVAC references | ≥3 active OEM accounts | Proves HVAC-specific domain knowledge |
Cost Structure: What You Actually Pay for
Tooling cost is the upfront investment — mold design, CNC machining, EDM, polishing, and first-article validation. For a typical single-cavity HVAC vent mold in P20 steel, expect $3,000–$8,000. A multi-cavity production mold for a filter frame in H13 steel runs $15,000–$40,000. These are 40–60% lower than equivalent Western tooling.
Per-part cost is driven by material, cycle time, and secondary operations. For a standard ABS air vent at 5,000 parts/month, per-part cost typically runs $0.80–$2.50 depending on complexity. Packaging, duty, and freight add 15–25% to landed cost. Total cost of ownership — including quality failures, rework, and tooling maintenance — is the correct comparison metric, not unit price alone.
“Chinese injection molding manufacturers offer 40–60% lower tooling costs than Western suppliers for equivalent HVAC components.”True
Lower labor rates, tooling infrastructure density, and material supply chain advantages in Guangdong and Zhejiang provinces allow Chinese manufacturers to deliver functionally equivalent P20 and H13 steel molds at significantly lower cost. The savings are greatest on mid-complexity tools in the $10,000–$50,000 range.
“Sourcing HVAC plastic parts from China always means sacrificing quality.”False
Производитель пластиковых деталей для HVAC в Китае: Руководство для покупателей.
Common HVAC Components and Their Manufacturing Requirements
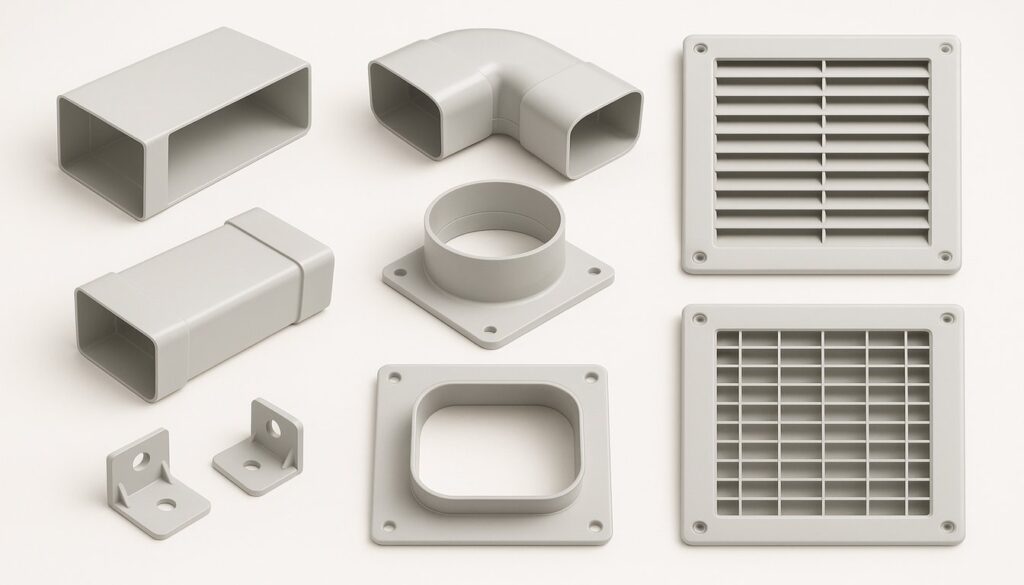
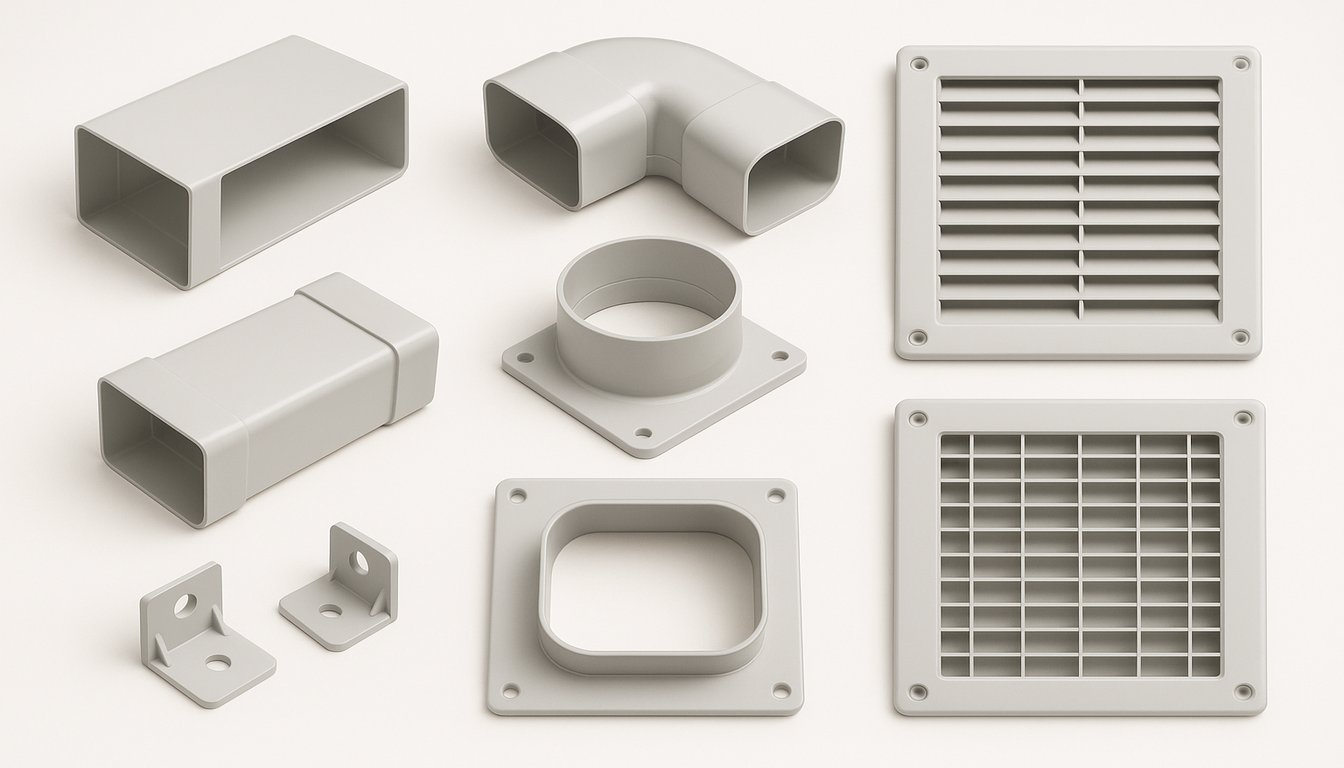
Air vents and grilles require consistent blade geometry and uniform wall thickness (1.5–2.5 mm). Multi-cavity molds (8–16 cavities) are standard for high-volume programs. Surface texture (matte or gloss) must match the specified VDI grade consistently across cavities.
Filter frames must hold dimensional tolerances of ±0.15 mm on gasket seating surfaces. Snap-fit features require ABS or PP at 40–60% nominal wall thickness — too thin and they fracture; too thick and the snap won’t deflect. DFM review before tooling is mandatory for this component class.
Electrical enclosures and control boxes must meet UL 94 V0 or V1. This requires specific flame-retardant ABS or PC/ABS formulations — not all suppliers stock compliant materials. Request the material data sheet and UL Yellow Card number before ordering. In our factory, we maintain stock of certified FR-ABS and PC/ABS for all enclosure programs.
HVACore’s HVAC Manufacturing Capabilities
HVACore specializes in injection-molded HVAC components for OEM and commercial construction supply chains. Our facility runs injection molding machines from 60 to 1,500 tons, covering the full range from small terminal clips to large plenum housings. We hold ISO 9001:2015 certification and maintain a dedicated HVAC applications team.
We support programs from prototype (single-cavity P20 molds, 4–6 week lead time) through production (multi-cavity H13 molds, 6–10 weeks). Every new program starts with a written DFM report — gate location, cooling analysis, wall thickness review, and draft angle confirmation — before steel is cut. This eliminates the most common first-article failure modes.
| Capability | Specification |
|---|---|
| Machine range | 60–1,500 ton clamping force |
| Mold steel grades | P20, H13, S136 |
| Certifications | ISO 9001:2015 |
| Lead time (new tooling) | 6–10 weeks |
| Minimum order | 5,000 parts |
Material range includes standard ABS and PP, UV-stabilized ASA for outdoor applications, glass-filled PP and nylon for structural brackets, and UL 94 V0-certified PC/ABS and FR-ABS for electrical enclosures. We ship to North America, Europe, and Australia with standard lead times and English-language documentation throughout.
Our quality team performs dimensional inspection on every first article using coordinate measuring machines (CMM) with tolerance resolution of ±0.005 mm. Critical dimensions — gasket grooves, snap-fit hooks, mounting hole centers — are verified against customer drawings before production release. For ongoing production, we maintain SPC charts on critical dimensions and report Cpk values with each delivery batch. Customers receive full dimensional reports, material certificates, and a certificate of conformance with every shipment, ensuring traceability from raw resin lot through finished part.
“DFM review before tooling is the single most effective way to reduce first-article failure rates.”True
In our factory, programs that include a written DFM report before steel cutting achieve first-article pass rates above 90%. Programs without DFM review average 3–4 revision cycles before release. The DFM cost — typically $0 when bundled with tooling — prevents weeks of rework.
“All Chinese plastic manufacturers can produce HVAC components to UL 94 flame rating requirements.”False
UL 94 compliance requires specific flame-retardant material formulations, documented lot traceability, and in some cases physical test coupons from actual production lots. Many general-purpose Chinese molders lack the material stock, documentation systems, or UL knowledge needed to reliably deliver V0 or V1 rated parts. HVAC buyers must verify compliance capability before awarding enclosure or plenum programs.
-
filter frames: Filter frames is a type of injection-molded HVAC enclosure that houses air filters in return-air ducts and air handling units, manufactured to dimensional tolerances of ±0.15 mm to prevent air bypass and maintain system filtration efficiency. ↩
-
ISO 9001: ISO 9001 is an international quality management standard certifying that a manufacturer maintains documented processes, inspection protocols, and continuous improvement systems — a baseline requirement for HVAC supply chain qualification. ↩
-
air vents: Air vents is a category of injection-molded HVAC components that regulate and direct airflow from ductwork into conditioned spaces, typically produced in ABS or ASA plastic for dimensional stability and UV resistance in residential and commercial systems. ↩
Frequently Asked Questions
What is the typical lead time when sourcing HVAC plastic parts from a Chinese manufacturer?
New tooling lead time is 6–10 weeks from approved design to first-article delivery. This includes mold design (1 week), CNC machining and EDM (3–4 weeks), polishing and assembly (1 week), and first-article inspection and report (1–2 weeks). Production lead time after tooling approval is 3–5 weeks for standard orders. Expedited schedules (4–6 weeks total) are available at 20–30% cost premium. Shipping to North America or Europe adds 2–4 weeks by sea, 5–7 business days by air. Contact HVACore to discuss your specific HVAC component requirements and receive a complete qualification package.
How do I verify that a Chinese HVAC manufacturer can meet UL 94 flame rating requirements?
Request the following documentation: UL Yellow Card for the specific resin lot being used (confirms the material formulation is UL-listed), material data sheet with UL 94 rating at the relevant thickness, and a sample UL 94 vertical burn test report from a recent production lot. Do not accept verbal assurances or generic catalog claims. For critical plenum applications requiring V0, consider commissioning independent testing at a UL-accredited laboratory. Reputable manufacturers will have this documentation readily available for any active FR program.
What quality documentation should I receive from an HVAC plastic parts manufacturer?
At a minimum: incoming material certificates (resin lot number, UL 94 rating, melt flow index), first-article inspection report (FAI or PPAP) with dimensional measurements against drawing tolerances, and ongoing production inspection records. For regulated applications (medical HVAC, cleanroom HVAC), add material traceability to raw polymer lot and a certificate of conformance per shipment. ISO 9001-certified manufacturers will have documented procedures for all of these; request the relevant procedure numbers during qualification. Contact HVACore to discuss your specific HVAC component requirements and receive a complete qualification package.
How does HVACore handle tooling ownership and mold maintenance for long-term programs?
All molds manufactured by HVACore are owned by the customer. Tooling ownership documentation is provided at delivery, and molds are stored on-site at no charge for active production programs. Preventive maintenance (cleaning, lubrication, wear inspection) is performed every 50,000–100,000 cycles and documented in the mold maintenance log. Customers receive maintenance reports annually. If a program becomes inactive, molds can be shipped to the customer or held in bonded storage at agreed rates. Contact HVACore to discuss your specific HVAC component requirements and receive a complete qualification package.
Can HVACore produce HVAC components that require both structural performance and UV resistance?
Yes. For outdoor HVAC applications requiring both structural strength and UV resistance — common in mini-split outdoor unit housings and rooftop equipment covers — we recommend glass-filled ASA (10–20% GF) or UV-stabilized ASA/ABS blends. These materials offer tensile strength above 40 MPa, pass ASTM G154 accelerated weathering at 2,000+ hours without significant color change or surface degradation, and are processable on standard injection molding equipment. We stock multiple ASA formulations and can provide UV weathering test data from production-equivalent samples before program launch.





