
それが吸気グリルです。グリルを作るには、溶けたプラスチックが鋼製のコアピンの周りで分岐し、反対側で再び合流しなければなりません。.
However, from a manufacturing standpoint, the window AC front panel is a geometric nightmare. It combines large flat surfaces (which show every imperfection) with intricate injection molded louvers (which disrupt plastic flow).
In my years managing HVAC aesthetic parts, the bezel has always been the bottleneck. You are constantly fighting a war between "airflow performance" (which needs open grilles) and "cosmetic perfection" (which hates the knit lines caused by those grilles). We often use High Impact Polystyrene (HIPS) for economy models or ABS for premium lines, but the processing challenges remain the same: hiding the evidence of how the plastic flowed into the mold.
Key Takeaways
- Front bezels require balancing structural snap-fits with Class-A aesthetic surfaces.
- "Weld lines" (knit lines) behind louvers are the most common defect and must be managed via gate placement.
- HIPS (High Impact Polystyrene) is the industry standard for cost, while ABS is used for high-gloss premium units.
- Sequential Valve Gating (SVG) is often required to move weld lines to non-visible areas.
Definition: The AC Front Bezel
In appliance plastic design, the bezel is the cosmetic and functional face of the unit. It serves three distinct roles:
- Intake: Holds the filter and allows room air to enter the evaporator.
- Discharge: Directs conditioned air out through adjustable louvers.
- Interface: Houses the control panel, display, and IR receiver.
Key Parameters for Bezel Molding
The parameters below reflect a standard 12,000 BTU window unit bezel molded in HIPS.
| Parameter | Typical Value | HVAC Manufacturing Context |
|---|---|---|
| Material | HIPS (High Impact Polystyrene) or ABS | HIPS is cost-effective and matte; ABS is used for high-gloss. Both must be UV stabilized to prevent yellowing. |
| Wall Thickness | 2.5mm – 3.2mm | Thick enough to prevent warping, thin enough to save weight. Ribs must be <60% of wall thickness to prevent sink marks. |
| Mold Temperature | 40°C – 60°C | Higher mold temps improve surface gloss and weld line strength but increase cycle time. |
| Gate Type | Hot Runner (Valve Gate) | Direct gating is necessary for such a large part to minimize pressure loss. |
| Draft Angle | 2° – 3° | Aggressive texturing (leather or matte grain) requires higher draft angles to release without drag marks. |
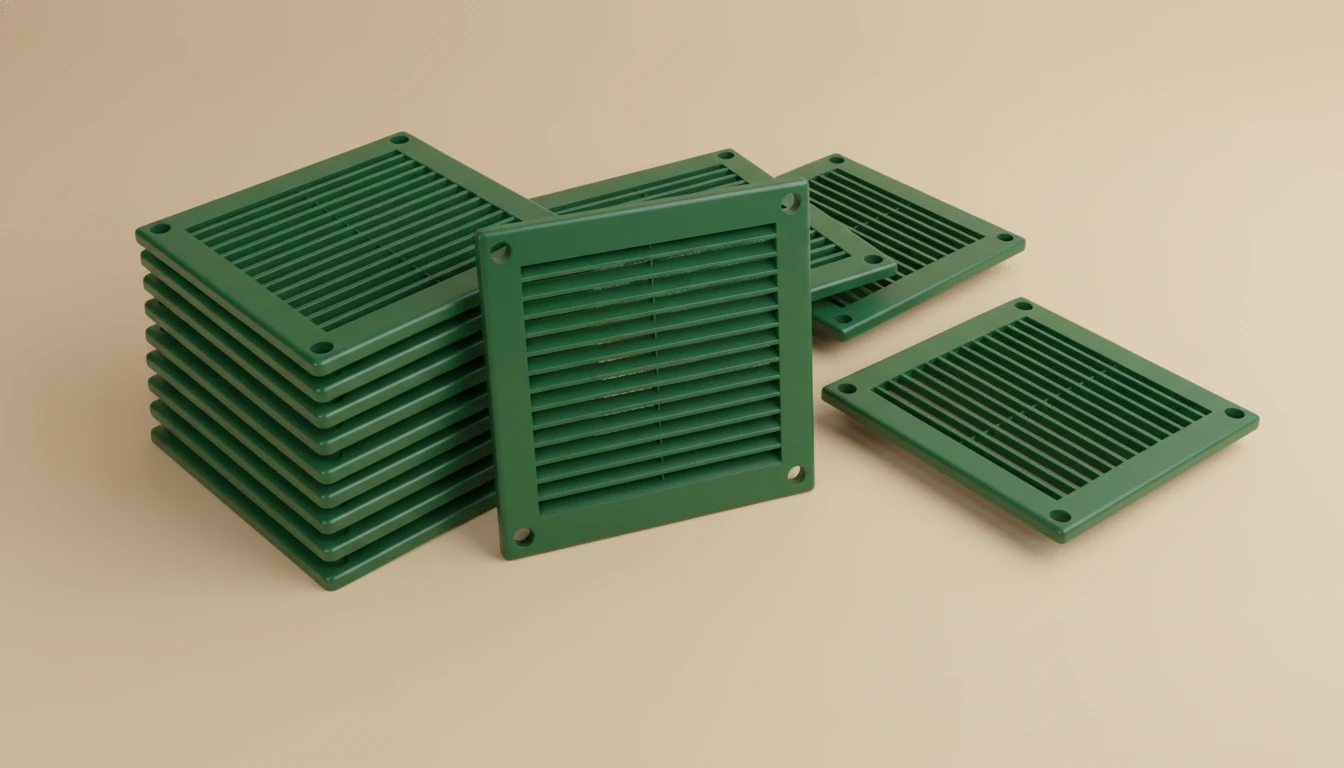
The "Louver Problem": Flow Lines vs. Aesthetics
The hardest part of air conditioner bezel molding is the intake grille. To make a grille, the molten plastic must split around the steel core pins and merge again on the other side.
仕上げ: フルマットテクスチャでフローマークを隠します。 Weld Line (or Knit Line).
- Structurally: This is a weak point. If a user pulls the filter out roughly, the grille can snap right at this line.
- Visually: It looks like a crack or a hair trapped in the plastic.
Real Factory Solution: Sequential Valve Gating (SVG)
On a premium 15,000 BTU project, we had massive weld lines right across the center logo area. The single gate approach wasn’t working.
The Fix:
We moved to a 5-drop Hot Runner system with Sequential Valve Gating.
- Drop 1 (Center): Opens first to fill the logo area (cleanest look).
- Drops 2 & 3 (Outer Edges): Open after the flow front passes them.
- Result: By timing the gates, we pushed the weld lines off the main face and into the corners where the bezel meets the metal chassis—completely hidden from the user.
Myth vs. Fact: Appliance Plastic Design
High gloss is unforgiving. It highlights every sink mark, scratch, and flow line. In mass production, we prefer a fine EDM texture (VDI 24-27) or a leather grain. It hides molding defects and fingerprint smudges, reducing scrap rates.
While discharge louvers are separate, the intake grille is almost always integral to the bezel. Molding it separately would double tooling costs and assembly time. We use complex slides (lifters) in the mold to create the undercuts for the intake.
Advantages and Disadvantages of Integrated Bezels
| Feature | Advantages | Disadvantages |
|---|---|---|
| Integral Snap Fits | Allows tool-free assembly on the line. Reduces screw count. | If a snap breaks during molding or assembly, the entire large part is scrap. |
| Material (HIPS) | Extremely low cost. Easy to paint or hot-stamp. | Lower chemical resistance than ABS. Can become brittle with UV exposure over 5+ years. |
| Complex Geometry | Can combine intake, discharge, and UI into one SKU. | Mold is massive and expensive. Requires a large tonnage machine (600T+) to clamp. |
Practical Tips for HVAC Aesthetic Parts
1. The "Sink Mark" Trap at Screw Bosses
Engineers love putting screw bosses (towers) on the back of the bezel to mount the PCB.
- The Issue: A thick screw boss on the back creates a dimple (sink mark) on the front face because the plastic shrinks more in that thick intersection.
- The Fix: We "core out" the base of the screw boss or add cosmetic distinct steps/grooves on the front face to disguise the sink mark. Design the cosmetic features around the internal mounting points.
2. Designing for Filter Removal
The most common warranty return on window units is broken filter tabs.
- Factory Insight: Do not mold rigid hooks for the filter. The bezel material (HIPS) fatigues. Instead, design the bezel with a slot, and mold the filter itself (PP material) with the flexible hook. Polypropylene hinges last forever; Polystyrene hinges snap.
3. Handling "Silver Streaks" (Splay)
If you see silvery streaks fanning out from the gate on a bezel, it’s not a mold issue—it’s moisture.
- Process Tip: HIPS is hygroscopic. Even if it looks dry, it needs 2 hours at 80°C in a desiccant dryer. Silver streaks on a black bezel are an instant reject.
HVAC Application Scenarios
- Economy Window Units:
- Material: HIPS.
- Finish: Full matte texture to hide flow lines.
- マスタリング ウィンドウ AC フロントベゼル:デザインと美学.
- Smart/Inverter Window Units:
- Material: ABS (High Gloss White).
- Finish: Requires "Heat & Cool" molding technology (Steam molding) to eliminate weld lines entirely for a glass-like finish. Includes a translucent section for hidden LED displays.
- Through-the-Wall (PTAC) Bezels:
- These are larger and thicker. We often add Glass Fiber (10%) to the HIPS to prevent the bezel from sagging over time due to the heat generated by the electric heater coil often found in PTACs.
Frequently Asked Questions (FAQ)
1. Why do older window AC bezels turn yellow?
This is UV degradation. Historically, manufacturers didn’t add enough UV stabilizers to the HIPS/ABS to save cost. Today, we add 2-3% UV masterbatch, but HIPS still yellows faster than ASA (Acrylonitrile Styrene Acrylate).
2. Can we paint the bezel to hide defects?
Yes, painting is common for "silver" or "champagne" models. However, painting adds $1-$2 per unit. For white units, we rely on molded-in color to keep costs down, which puts the pressure back on the molder to minimize defects.
3. How do you clean the flash from the louver slats?
If the mold is built correctly, there should be zero flash. Deflashing louvers by hand is impossible without leaving scratch marks. We use high-precision CNC machining for the mold cores to ensuring a "steel-safe" shutoff that prevents plastic leakage.
4. Why are the snap-fits so stiff?
This is often a design error regarding the material’s Flexural Modulus. Engineers design snaps based on Nylon data, but use HIPS. We often have to thin out the root of the snap clip during tool tuning to make it flexible enough for the consumer to operate.
5. What is the biggest molding risk for large bezels?
Warpage. A long, flat bezel tends to bow in the middle like a banana. We solve this by adjusting the cooling channel layout in the mold to ensure the front and back of the part cool at the exact same rate.
Technical Summary
Designing and molding a window AC front panel is a masterclass in compromise. You are using a low-cost material (HIPS) to create a high-value aesthetic part. The primary technical challenge is managing the flow front through injection molded louvers to minimize weld lines. Success relies on advanced sequential valve gating, precise mold temperature control, and strategic use of surface textures. For the HVAC manufacturing engineer, the goal is a bezel that snaps on easily, stays flat, and withstands years of UV exposure without becoming brittle.





