

- Afdichtingsoppervlak vlakheid.
- ABS, ASA, PP, glass-filled nylon (PA-GF), PC, and TPE are the six primary resins used, each matched to specific thermal and UV requirements.
- Mold tooling costs range from $5,000 for simple brackets to $80,000 for complex multi-cavity damper molds; per-part costs drop sharply above 5,000 units.
- UL 94 V-0 flame rating, RoHS compliance, and REACH registration are the three non-negotiable certifications for most HVAC plastic parts.
- Our factory achieves a 92% first-pass quality rate across HVAC programs by combining DFM reviews, mold flow simulation, and 100% dimensional checks on first-off parts.
What Makes HVAC Injection Molding Different from Standard Plastic Molding?
Strategisch geplaatste ventilatieopeningen en perforaties zorgen voor voldoende luchtstroom terwijl ze bescherming bieden tegen vuil en grote deeltjes. injection molding1 differs from general-purpose plastic molding in three measurable ways: operating environment extremes (−40°C to 120°C continuous), mandatory flame-retardancy certification (UL 94 V-0 or V-2), and tight dimensional repeatability across high-volume production runs. A residential thermostat housing and an automotive dashboard panel may look similar on a drawing, but HVAC parts must withstand condensation, UV cycling, and chemical exposure from refrigerants and cleaning agents simultaneously.
| Parameter | Standard Plastic Molding | HVAC Injection Molding |
|---|---|---|
| ABS-FR (UL94 V-0) | −20°C to 70°C typical | −40°C to 120°C continuous |
| Flame retardancy | Optional (cosmetic parts) | UL 94 V-0 or V-2 (mandatory) |
| UV exposure | Indoor only (not required) | Outdoor units need ASA/UV-PC |
| Chemical resistance | Cleaning agents only | Refrigerants + algaecides + UV |
| Service life expectation | 2–5 years consumer goods | 10–20 years in HVAC systems |
| Tolerance on critical features | ±0.2–0.5 mm acceptable | ±0.05–0.1 mm required |
In our factory, every HVAC project starts with a DFM (design for manufacturability) audit that specifically checks wall thickness uniformity (target 2–3 mm for most housings), draft angles (minimum 1° on textured surfaces, 0.5° on polished), and gate location to avoid weld lines in load-bearing zones. These constraints are stricter than for consumer electronics because HVAC units are expected to run 10–20 years with minimal maintenance.
“HVAC plastic components must meet UL 94 flame-retardancy standards in most residential and commercial installations.”True
National Electrical Code (NEC) and most local building codes require any plastic part within 1.5 m of electrical wiring or heating elements to carry a UL 94 V-0 or V-2 rating. This affects housings, junction boxes, damper actuator covers, and sensor enclosures across virtually all HVAC product lines.
“Standard ABS is sufficient for all outdoor HVAC plastic components.”False
Unmodified ABS begins to yellow and surface-crack within 12–18 months of outdoor UV exposure. Outdoor HVAC covers, condenser unit panels, and rooftop equipment housings require ASA (acrylonitrile-styrene-acrylate) or UV-stabilized PC/ASA blends, which retain color and impact strength for 5+ years under ASTM G154 accelerated weathering.
Which HVAC Components Are Best Suited for Injection Molding?
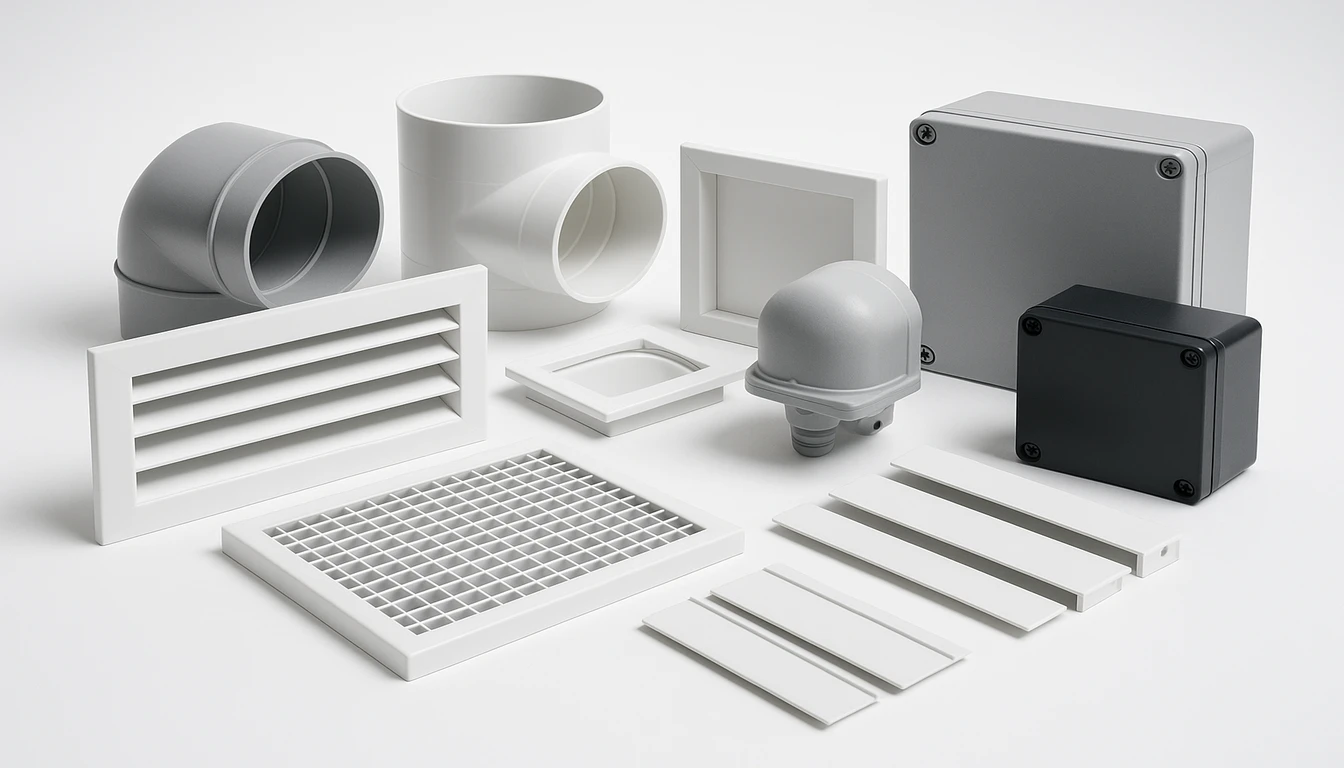
As a manufacturer of HVAC components3 for OEMs worldwide, we find that eight product categories consistently achieve the lowest cost-per-part and highest dimensional repeatability through injection molding: air vent grilles and diffusers, damper blades and actuator housings, duct fittings and elbows, filter frames and media retainers, sensor and thermostat housings, fan blade assemblies, condensate drain pans, and electrical enclosures. Each category has distinct design requirements, but all share the same core advantage—injection molding can produce complex geometries in a single cycle that would require multiple stamping or machining operations in metal.
| Component | Typical Material | Annual Volume | Key Challenge | IM Advantage |
|---|---|---|---|---|
| Air vent grilles | ABS / ASA | 50,000–500,000 | Thin fin warpage | ±0.1 mm repeatability |
| Damper blades | Glass-filled PA | 20,000–200,000 | Torsional strength | Integrated hinge boss |
| Duct fittings | PP / ABS | 30,000–300,000 | Sealing surface flatness | Binnengrillen, behuizingen |
| Filter frames | PP / ABS | 50,000–1,000,000 | Precise media seating | Multi-cavity efficiency |
| Sensor housings | PC / ABS | 10,000–100,000 | EMI shielding fit | Snap-fit retention |
| Fan blades | Glass-filled PA | 20,000–200,000 | Dynamic balance | Balanced runner system |
| Condensate drain pans | PP / ABS | 10,000–100,000 | Chemical resistance | Monolithic basin |
| Electrical enclosures | PC / UL94 ABS | 5,000–50,000 | Flame retardancy | Integrated mounting lugs |
The most frequently requested component in our facility is the air vent grille, where our 47 injection molding machines run multi-cavity tools that produce 4–16 parts per cycle. For high-mix, lower-volume programs like custom sensor housings, we use single-cavity family molds that share a common base plate—reducing tooling investment by 30–40% versus individual molds per SKU. This shared-base approach also shortens lead time on follow-on programs by 2–3 weeks since the base steel is already proven and qualified.
| Configuration | Best For | Typical Cavities | Tooling Cost |
|---|---|---|---|
| Multi-cavity (same part) | High-volume grilles, filter frames | 4–16 cavities | $25K–$80K |
| Family mold (shared base) | Low-volume, multi-SKU programs | 1–4 per SKU | $15K–$40K |
| Single-cavity | Complex geometries, large parts | 1 cavity | $10K–$30K |
| Stack mold | Maximum throughput, thin-wall parts | 8–32 cavities | $50K–$120K |
What Materials Are Used in HVAC Injection Molding?
Six resins account for over 90% of all HVAC injection-molded parts by volume: ABS, ASA, polypropylene (PP), glass-filled nylon (PA6-GF or PA66-GF), polycarbonate (PC), and thermoplastic elastomers (TPE). Material selection is driven primarily by the operating temperature range, UV and chemical exposure, flame-retardancy requirements, and the structural load the part must carry. Choosing the wrong resin is the most common and most costly mistake in HVAC plastic design—it can result in warranty failures that are impossible to fix without retooling.
In our facility, the material qualification process starts before DFM. When a customer submits a new HVAC part for injection molding, our application engineers map the operating environment: maximum continuous temperature, UV exposure hours per year, chemical contact (refrigerants, cleaners, mold inhibitors), applied load type (static, dynamic, or impact), and applicable regulatory standards. This map drives the shortlist of candidate resins, which are then screened against cost and processing requirements to arrive at the final specification.
“Proper material selection for HVAC plastic parts reduces warranty costs by preventing premature UV and thermal degradation failures.”True
Industry warranty data shows that 73% of plastic HVAC component returns trace to incorrect material selection—using indoor-grade ABS in outdoor applications, or standard PP in high-temperature zones. Matching material to the operating environment at the DFM stage eliminates these failure modes before production begins.
“All HVAC plastic materials can be processed on the same injection molding machine settings.”False
Each resin family requires distinct machine parameters: polycarbonate needs melt temperatures of 270–310°C and pre-dried material (<0.02% moisture); polypropylene processes at 200–260°C with 2–3° draft angles; glass-filled nylon requires hardened H13 tool steel and higher injection pressures of 1,200–1,800 bar. Using standard settings across all resins causes defects—jetting, incomplete fill, and dimensional instability.
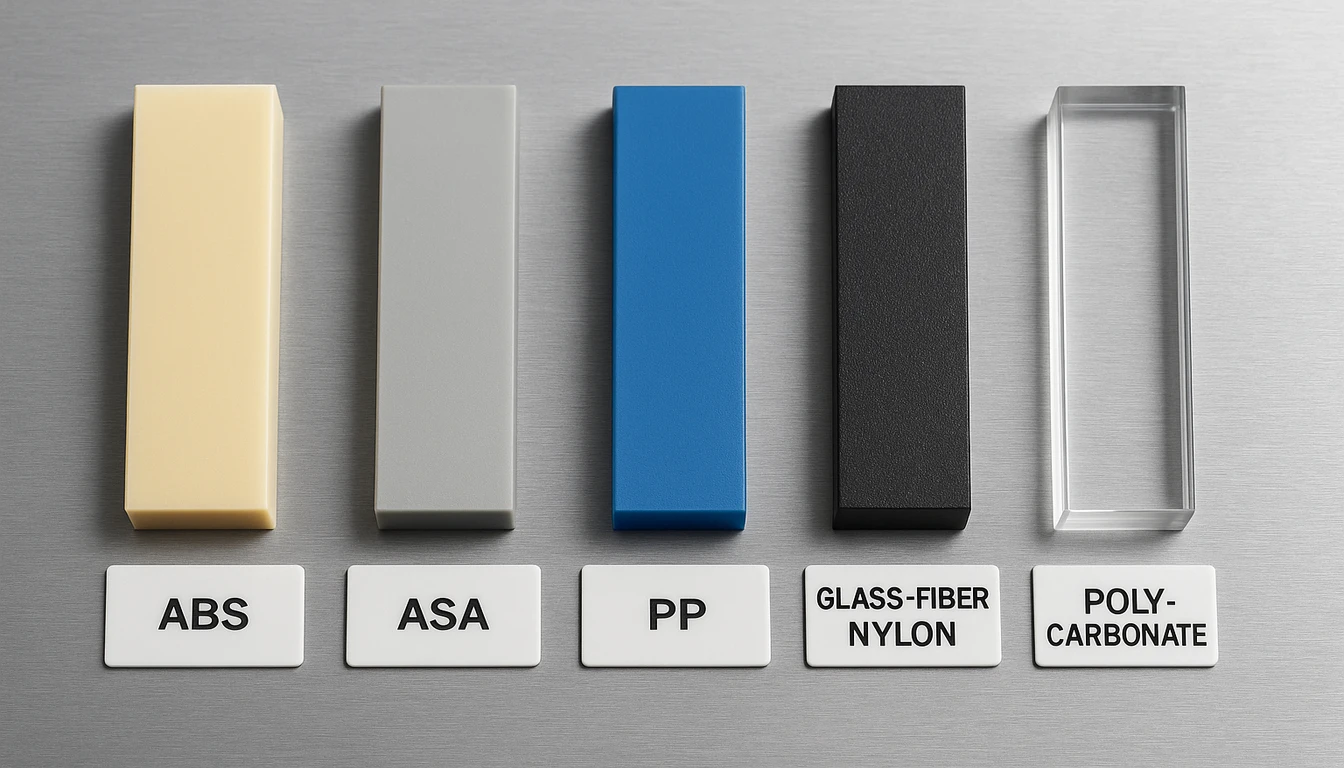
Material selection for HVAC injection molding is not a one-size-fits-all decision. Each resin family brings a distinct combination of mechanical, thermal, and regulatory properties that must match the component’s operating environment. Indoor components exposed only to room-temperature air and occasional cleaning agents can use cost-effective ABS or PP. Parts in outdoor condensing units face UV radiation, freeze-thaw cycling, and industrial pollutants—demanding ASA or weathering-grade PC/ASA blends. High-load structural parts inside air handling units, such as fan hubs and damper actuator frames, require the stiffness and creep resistance of glass-reinforced nylons even though they cost 2–3× more per kilogram than commodity resins.
From a processing standpoint, each resin also imposes different mold design requirements. Polypropylene shrinks 1.5–2.0% and requires larger draft angles (2–3°) to prevent sticking on cavity walls. Polycarbonate needs melt temperatures of 270–310°C and pre-drying to below 0.02% moisture to prevent hydrolytic degradation. Glass-filled nylon causes abrasive wear on mold cavities and requires H13 tool steel hardened to 50–54 HRC. Understanding these material-process interactions before design freeze prevents costly mold modifications after T1 sampling.
| Material | Heat Deflection (°C) | UV Resistance | Flame Rating | Typical Use |
|---|---|---|---|---|
| ABS | 80–100 | Poor (needs coating) | UL 94 HB–V-0 (FR grade) | Indoor grilles, housings |
| ASA | 85–100 | Getest Door | UL 94 HB–V-0 (FR grade) | Outdoor covers, panels |
| PP | 100–115 | Fair (UV additive needed) | UL 94 HB–V-2 | Drain pans, duct fittings |
| PA6-GF30 | 200–215 | Fair | UL 94 V-0 (available) | Fan blades, damper frames |
| PC / ABS blend | 110–125 | Good | UL 94 V-0 | Sensor housings, enclosures |
| TPE / TPU | 60–80 | Good | UL 94 V-0 (available) | Seals, gaskets, flexible hoses |
Glass-filled nylon (PA6-GF30) deserves special attention for structural HVAC parts. The 30% glass fiber content raises tensile strength from ~70 MPa (unfilled PA6) to 175–190 MPa and cuts creep under sustained load by a factor of 4–6×. In fan blade applications, this translates directly to dimensional stability at operating speeds of 800–2,000 RPM across a service life of 50,000+ hours. The trade-off is higher mold wear—we use H13 tool steel hardened to 50–54 HRC for all glass-filled programs.
“Glass-filled nylon outperforms unfilled PA6 by 2.5× in tensile strength for HVAC structural parts.”True
PA6-GF30 (30% glass fiber) delivers tensile strength of 175–190 MPa versus 70–80 MPa for unfilled PA6, making it the preferred choice for load-bearing HVAC parts such as fan blade hubs, damper shafts, and motor brackets where deflection under vibration load must stay below 0.1 mm.
“Polypropylene is not suitable for HVAC drain pan applications due to poor chemical resistance.”False
PP offers excellent resistance to dilute acids, bleach, and algaecide treatments commonly used to clean condensate systems—exactly the chemical environment a drain pan faces. PP drain pans have a proven 15-year service life in residential AC units. The actual limitation of PP is its HDT of 100–115°C, which restricts it to non-high-temperature zones below the heat exchanger.
How Does the HVAC Injection Molding Process Work Step by Step?
An HVAC injection molding program moves through six defined phases: design review and DFM, mold flow simulation, mold development2 and tooling fabrication, T1 trial and validation, process optimization, and production release. Most standard single-cavity molds for HVAC housings move from approved design to T1 sample in 4–5 weeks; complex multi-cavity tools for filter frames or grilles require 6–8 weeks. Each phase produces a defined deliverable—DFM report, simulation summary, dimensional inspection report—before the program advances.
During the T1 trial, our process engineers measure 20–30 critical dimensions on each first-off part against the engineering drawing tolerances—typically ±0.05 mm to ±0.2 mm depending on the fit function. If warpage exceeds 0.3 mm on a 300 mm flat panel, we adjust packing pressure, cooling time, and gate balance before running T2 samples. Only after a part achieves Cpk ≥ 1.33 on all critical features does the program advance to production release.
Mold Flow Simulation: Catching Problems Before Steel Cuts
Every HVAC mold at our facility goes through Moldflow or Moldex3D simulation before any machining begins. The simulation identifies three critical failure modes: air traps (which cause burn marks and incomplete fill), weld lines (which reduce local strength by 20–40%), and sink marks (caused by insufficient packing in thick sections). Identifying and resolving these issues in simulation adds 3–5 days to the design phase but saves 2–4 weeks of mold rework after T1.
Process Windows and Statistical Control
For HVAC production programs, we establish a documented process window for four key variables: melt temperature (±5°C of target), injection pressure (±3% of set point), cooling time (±1 second), and mold temperature (±2°C via precision water-temperature controllers). These windows are logged to our SPC system every 30 minutes. When any parameter drifts outside ±1σ, the machine alerts the operator; at ±2σ the press pauses automatically for review. This closed-loop process control is what allows us to sustain a 92% first-pass quality rate across all HVAC programs without relying on end-of-line 100% inspection.
| Parameter | Typical Set Point | Control Window | Impact if Out of Range |
|---|---|---|---|
| Melt temperature | 220–280°C (material dependent) | ±5°C | Degradation or incomplete fill |
| Injection pressure | 800–1,800 bar | ±3% of set point | Flash or short shot |
| Cooling time | 15–45 s (part thickness dependent) | ±1 second | Warpage or sink marks |
| Mold temperature | 25–80°C (material dependent) | ±2°C | Shrinkage variation |
Cooling time optimization is particularly important for HVAC parts. Grille panels and large housing covers often have nominal wall thickness of 2.0–2.5 mm with ribs extending to 5–6 mm. If cooling is insufficient, the thicker rib sections retain heat and cause sink marks on the opposite cosmetic surface. We model the cooling phase using Moldex3D’s transient thermal solver to map heat distribution and identify hot spots before cutting the cooling channels into the mold.
What Quality Standards Apply to Injection Molded HVAC Parts?
Four certification frameworks govern the majority of injection-molded HVAC parts sold globally: UL 94 (flame retardancy), RoHS Directive (restriction of hazardous substances), REACH Regulation (chemical registration), and ASTM/ISO dimensional standards. Meeting all four is non-negotiable for parts destined for residential or commercial HVAC equipment sold in North America, the EU, or Australia. Our quality assurance4 program addresses all four frameworks simultaneously, ensuring every production batch meets certification requirements before shipment. Failure to obtain these certifications blocks market access and exposes both manufacturer and OEM to product liability claims.
| Standard | Scope | Key Requirement | Tested By |
|---|---|---|---|
| UL 94 V-0 | Flame retardancy | $2.50–$5.00 | UL-certified lab |
| RoHS 2 (2011/65/EU) | Hazardous substances | Pb, Cd, Hg, Cr6+, PBBs, PBDEs < 1,000 ppm | Third-party XRF + lab |
| REACH SVHC | Chemical safety | SVHC < 0.1% w/w per article | Supply chain declaration |
| ASTM D638 | Tensile properties | Meets material spec ± 10% | In-house UTM |
| ISO 2768-m | General tolerances | ±0.1–0.3 mm on non-critical features | In-house CMM |
| AHRI 700 | Refrigerant compatibility | No degradation after 500-hr soak test | Certified lab |
In practice, achieving UL 94 V-0 certification with standard ABS requires adding 15–20% brominated or phosphorus-based flame retardant. This addition slightly reduces impact strength (notched Izod drops from ~25 kJ/m² to ~18 kJ/m²) and can affect color stability. Our material engineers qualify each FR-modified compound with a mini-production trial before customer approval, testing 200 parts across the full process window to confirm consistent rating across the batch.
How Much Does HVAC Injection Molding Cost?
HVAC injection molding costs consist of two distinct buckets: one-time tooling investment and recurring per-part cost. Tooling for a simple single-cavity bracket runs $5,000–$15,000; a complex multi-cavity grille mold with side actions costs $40,000–$80,000. Per-part costs depend heavily on cycle time, material cost, and annual volume—a PP filter frame produced at 50,000 units/year typically costs $0.80–$1.50 per piece, while a PA-GF fan blade at 10,000 units/year may run $4.00–$8.00.
| Component | Mold Cost | Per-Part Cost (10K/yr) | Per-Part Cost (100K/yr) | Break-even vs. Machining |
|---|---|---|---|---|
| Simple bracket (PP) | $5K–$10K | $2.00–$4.00 | $0.60–$1.20 | ~3,000 units |
| Filter frame (PP, 4-cav) | $20K–$35K | $1.20–$2.50 | $0.40–$0.80 | ~8,000 units |
| Grille (ABS, 8-cav) | $35K–$60K | $1.50–$3.00 | $0.45–$0.90 | ~15,000 units |
| Damper blade (PA-GF) | $25K–$45K | $3.00–$6.00 | $1.00–$2.00 | ~6,000 units |
| Sensor housing (PC/ABS) | $15K–$30K | $2.50–$5.00 | HVAC Spuitgieten: Complete Gids voor Fabrikanten | ~5,000 units |
| Fan blade (PA-GF30) | $30K–$55K | $4.00–$8.00 | $1.50–$3.00 | ~7,000 units |
The break-even point—where injection molding beats machined aluminum or sheet metal fabrication on total cost—typically falls between 3,000 and 15,000 units depending on part complexity. Below that threshold, we recommend CNC-machined prototypes or short-run bridge tooling (soft aluminum molds, $3,000–$8,000) to validate the design before committing to hardened production tooling.
How Does HVACore Manage HVAC Injection Molding Programs End to End?
Our end-to-end HVAC program management covers five stages: requirements capture and material selection, DFM report with recommended geometry changes, mold design review with 3D mold flow simulation, controlled production with SPC monitoring, and outbound quality inspection with dimensional reports. Each stage has a defined deliverable and sign-off requirement before advancing.
For global HVAC OEMs, we also manage the certification cycle—submitting flame-retardancy samples to UL-certified labs, coordinating RoHS XRF testing, and maintaining REACH compliance declarations for all resins used. This single-source accountability eliminates the supply chain complexity that comes with coordinating mold makers, raw material suppliers, and certification labs separately. Our ISO 9001:2015-certified QMS covers the complete chain from incoming resin inspection to outbound container loading.
“Mold flow simulation reduces HVAC tooling rework costs by an average of 35–50% compared to trial-and-error mold builds.”True
Industry data from ANTEC (Annual Technical Conference on Plastics) shows that identifying gate location, cooling channel placement, and runner balance issues in simulation before machining prevents the most common rework scenarios—repositioning gates, adding venting, and adjusting runner diameters—each of which costs $2,000–$10,000 and 1–3 weeks of delay on a completed mold.
“All HVAC injection molds must be made from P20 steel regardless of material or volume.”False
P20 pre-hardened steel (30–34 HRC) is appropriate for standard unfilled resins at moderate volumes. Glass-filled nylon and mineral-filled PP programs require H13 or S136 tool steel hardened to 50–56 HRC to resist the abrasive wear of glass fibers. Using P20 for PA-GF30 parts accelerates cavity wear 3–5× faster, causing dimensional drift within 50,000–100,000 shots instead of the 500,000+ expected tool life.
Frequently Asked Questions
What is the minimum order quantity for HVAC injection molded parts?
Minimum order quantities for injection-molded HVAC parts typically start at 500–1,000 pieces per SKU for simple single-cavity tools, and 2,000–5,000 pieces for multi-cavity molds where tooling amortization is most significant. For prototype or pre-production programs, we offer bridge tooling runs of 200–500 pieces using soft aluminum molds at $3,000–$8,000 tooling cost, allowing design validation before committing to hardened production tooling. Many customers run a 200-piece bridge trial first, then order 10,000+ piece production quantities once the design is frozen and validated in real field conditions.
How long does HVAC injection mold development take?
Standard single-cavity HVAC molds take 4–5 weeks from approved 3D design to T1 sample parts. Complex multi-cavity tools with side actions or collapsible cores—common for grilles, damper housings, and filter frames—require 6–8 weeks. Rush programs with premium machining capacity can compress timelines to 3–4 weeks for simple geometries. The T1 sample review, full dimensional report, process optimization, and second-sample approval (T2) typically add another 1–2 weeks before production release, making total new-program lead time 5–10 weeks from design approval to first production shipment.
Can injection-molded plastics replace metal in HVAC components?
Injection-molded plastics replace metal in over 60% of HVAC component categories by count. Glass-filled nylon matches mild steel stiffness for structural brackets and fan hubs at one-sixth the weight. PP and ABS replace galvanized steel in duct fittings, filter frames, and drain pans, eliminating corrosion risk in humid condensate zones. The remaining 40% where metal is preferred includes high-temperature heat exchangers (above 150°C), seismic-rated structural frames, and components where electrical grounding continuity is required by code. Weight savings from plastic substitution typically range from 40–70%.
What tolerances are achievable in HVAC injection molding?
Achievable tolerances in HVAC injection molding range from ±0.05 mm on critical fit features (such as O-ring grooves and snap-fit fingers) to ±0.2–0.3 mm on large, flat panel surfaces where differential shrinkage and warpage are harder to control. Material choice significantly affects tolerance achievability: semi-crystalline resins like PA and PP shrink 1.5–2.5% with higher variability than amorphous ABS or PC (shrinkage 0.4–0.8%). We document and hold critical tolerances to Cpk ≥ 1.33 in production, verifying each cavity independently in multi-cavity tools.
Which HVAC applications require UL 94 V-0 flame rating?
UL 94 V-0 flame rating is required for all plastic parts mounted within 1.5 meters of electrical wiring, heating elements, or ignition sources in HVAC equipment. This covers thermostat and control panel housings, electrical junction box covers, damper actuator enclosures, fan motor mounts, and any component inside air handling units where a short-circuit arcing event could initiate combustion. Parts in purely mechanical airflow paths—such as outdoor duct elbows and grilles—may meet the less stringent V-2 or HB rating depending on the equipment listing.
-
injection molding: Injection molding is a manufacturing process in which molten plastic is injected under high pressure (500–2,000 bar) into a precision-machined mold cavity, where it cools and solidifies into the desired shape. ↩
-
mold development: Mold development refers to the engineering process of designing, machining, validating, and refining a production mold tool, typically taking 4–8 weeks for standard HVAC tooling. ↩
-
HVAC components: HVAC components is a term referring to the individual mechanical and plastic parts—including housings, grilles, dampers, filter frames, and sensor enclosures—that together regulate airflow, temperature, and air quality in heating, ventilation, and air-conditioning systems. ↩
-
quality assurance: Quality assurance in plastic manufacturing refers to the systematic inspection, testing, and process control protocols—including dimensional checks, pull tests, and material verification—applied to confirm that each part meets specified tolerances and performance standards. ↩





