
Compression Molding Coeficiente de atrito baixo de 0,15-0,25 com excelentes propriedades de autolubrificação
Precision compression molding solutions for durable HVAC components. From thermosetting plastics to complex geometries, we deliver quality parts with ±0.1mm accuracy and full compliance standards.
Table of Contents
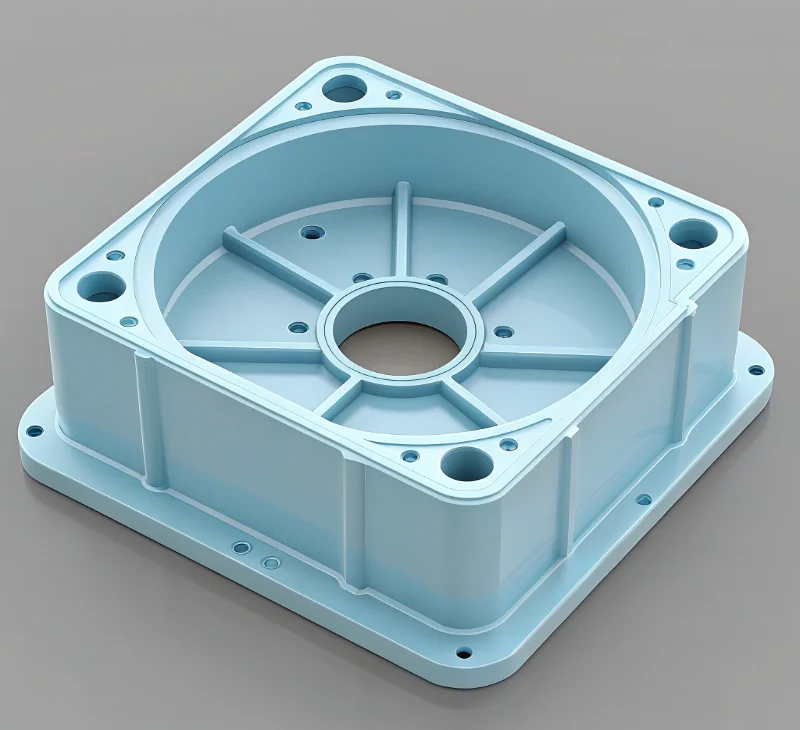
What is Compression Molding?
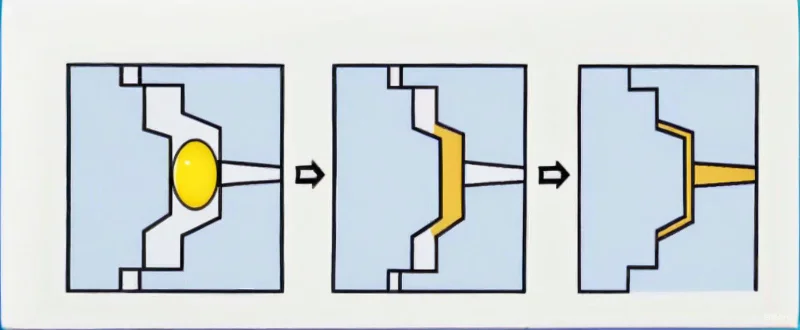
Compression molding is a high-pressure molding process fundamentally defined as a method where a pre-measured amount of molding material (often referred to as a "charge" or "preform") is placed directly into a heated, open mold cavity. The mold is then closed, applying immense pressure and sustained heat to force the material to soften, flow, and completely fill the cavity, ultimately curing and solidifying it through chemical cross-linking or physical cooling to create a product of the desired shape.
Key Process: Material Placement → Mold Closure → Heat & Pressure → Curing → Final Component
Process Characteristics
High Pressure Application
The process applies significant pressure to force material into every corner of the mold cavity, ensuring complete filling and eliminating voids or air pockets.
Why it's crucial for HVAC: High pressure ensures dense, strong components that can withstand the demanding conditions of HVAC systems without deformation.
Thermal Curing Process
Controlled heat application triggers chemical cross-linking in thermosetting materials, creating permanent molecular bonds that won't melt under operational temperatures.
Why it's important for HVAC: Thermal curing produces components that maintain their shape and properties even when exposed to extreme temperature variations in HVAC systems.
Material Efficiency
Precise material placement minimizes waste, as only the exact amount needed for each part is used, making it an economical choice for high-value engineering materials.
Why it's important for HVAC: Material efficiency reduces production costs while maintaining the high-quality standards required for critical HVAC components.
Materials & Applications
Thermosetting Plastics
The process is ideal for materials like phenolic resins, epoxy resins, and unsaturated polyester resins that require heat-induced chemical cross-linking for final properties.
Why it's crucial for HVAC: These materials offer superior heat resistance, electrical insulation, and chemical stability essential for HVAC components operating in harsh environments.
Fiber Reinforced Composites
Compression molding excels with SMC/BMC materials, creating components with exceptional strength-to-weight ratios and dimensional stability.
Why it's crucial for HVAC: Fiber reinforcement provides the structural integrity needed for components that must maintain shape under pressure and temperature fluctuations.
HVAC Critical Components
The process produces high-strength, chemically resistant parts ideal for HVAC applications where durability and performance are non-negotiable.
Why it's crucial for HVAC: These components form the backbone of reliable HVAC systems, ensuring long-term operation with minimal maintenance requirements.
What HVAC Plastic Parts Can be Made From Compression Molding?
Compression molding technology enables the production of high-performance HVAC plastic components with superior mechanical properties, thermal stability, and chemical resistance. From lightweight fan impellers that reduce energy consumption by 15-20% to corrosion-resistant valve bodies capable of withstanding 2.5MPa pressure, compression molded parts offer significant advantages over traditional materials. The technology supports precise dimensional control (±0.1mm), excellent surface finishes (Ra 1.6μm), and can create large integrated components up to 2.5m×1.8m. With material options including glass fiber reinforced phenolic resins and SMC composites, these components deliver exceptional durability, with service lives exceeding 20 years in outdoor applications while reducing weight by 35-60% compared to metal alternatives.
Key Applications: Fan Systems • Valve Components • Structural Housings • Sealing Systems • Electrical Insulation
1. Fan and Air Handling Systems
Fan Impellers & Housings
Manufactured using 30%-40% glass fiber reinforced phenolic resin (PF-GF30) or SMC materials with dimensional tolerance control of ±0.1mm.
-
•
Dynamic balance precision reaches G2.5 level with maximum speed up to 3000 RPM
-
•
40%-60% weight reduction compared to traditional aluminum alloy impellers, reducing motor startup load by approximately 25%
-
•
Overall energy consumption reduced by 15%-20% with fatigue strength exceeding 10^7 cycles
-
•
Stable mechanical performance maintained in temperature range from -40℃ to 120℃
Flow Guides & Fairings
Made from low shrinkage (<0.2%) epoxy molding compounds with surface roughness Ra reaching 1.6μm.
-
•
CFD-optimized design improves airflow distribution uniformity by 30% and reduces vortex loss by 25%
-
•
System overall energy efficiency ratio (EER) improved by 8%-12%
-
•
Smooth inner surface reduces air resistance coefficient to below 0.02 with airflow output optimization rate over 95%
-
•
Noise level reduced by 3-5dB(A)
2. Valves and Control Components
Valve Bodies & Discs
Using phenolic resin (PF) or epoxy resin (EP) molding compounds with working pressure up to 2.5MPa and burst pressure exceeding 7.5MPa.
-
•
Low friction coefficient of 0.15-0.25 with excellent self-lubricating properties
-
•
Resina Fenólica (Termoendurecível) <0.05mm after 100,000 switching operations
-
•
Temperature resistance range from -60℃ to 150℃, compatible with R134a, R410A, R32 and other refrigerants
Actuator Housings & Control Panels
Featuring UL94 V-0 flame retardancy rating with CTI (Comparative Tracking Index) >600V and dielectric strength >20kV/mm.
-
•
Protection rating up to IP65 with operating temperature range -40℃ to 125℃
-
•
Water absorption rate <0.1%, ensuring stable electrical performance in humid environments
-
•
Effectively shields electromagnetic interference (EMI) to protect internal microprocessors and sensors
3. Housings and Structural Components
Outdoor Unit Casings
Made from SMC composite materials with integrated molding, maximum size up to 2.5m×1.8m, adjustable wall thickness 3-8mm.
-
•
Impact strength >60kJ/m², tensile strength >80MPa, bending strength >150MPa
-
•
UV resistance meets ASTM G154 standard with service life exceeding 20 years
-
•
35% weight reduction compared to sheet metal casings with 10 times improved corrosion resistance
-
•
No periodic painting maintenance required
Internal Brackets & Mounting Bases
Utilizing 40% glass fiber reinforced materials with compressive strength >200MPa and elastic modulus >10GPa.
-
•
Can replace Q235 steel with weight reduction effect over 50%
-
•
Mounting hole position accuracy ±0.05mm ensuring assembly precision
-
•
Low thermal expansion coefficient of 10-15×10^-6/℃, good compatibility with metal components
-
•
Heat deflection temperature (HDT) >180℃
4. Sealing and Connection Systems
Flanges & Sealing Gaskets
Made from high-temperature modified phenolic resin with long-term service temperature -60℃ to 200℃, short-term resistance up to 260℃.
-
•
Compression set <10% with compression recovery rate >90%
-
•
Excellent chemical corrosion resistance to refrigerants, freezer oils, cleaning agents and other chemical media
-
•
Sealing pressure up to 3.0MPa ensuring zero system leakage
Pipe Connectors & Fittings
Integrated molding design with wall thickness uniformity controlled within ±0.1mm.
-
•
Burst pressure >8.0MPa with vacuum sealing capability up to -0.095MPa
-
•
Special formula materials with linear expansion coefficient close to copper pipes (17×10^-6/℃), reducing thermal stress
-
•
Inner surface smoothness Ra<0.8μm, reducing fluid resistance and preventing impurity deposition
5. Electrical and Insulation Components
Terminal Boxes & Connection Blocks
With dielectric strength >25kV/mm, volume resistivity >10^14Ω·cm, and surface resistivity >10^13Ω.
-
•
Arc resistance >180 seconds with UL94 V-0 flame retardancy rating
-
•
Operating temperature -55℃ to 130℃ with heat deflection temperature >200℃
-
•
Passes IEC 60695-2-11 glow wire test (GWIT: 775℃) ensuring electrical safety
Motor Insulation Components
Insulation class reaches H level (180℃) with insulation resistance >100MΩ in 95% relative humidity at 85℃ environment.
-
•
Voltage resistance test can withstand 2500V AC/1min without breakdown
-
•
Excellent corona resistance performance, capable of withstanding 10^6 corona impacts
-
•
Service life extended by 3-5 times compared to traditional insulation materials
-
•
Motor efficiency improved by 2%-3%
What Plastic Material can Used in HVAC Compression Process?
HVAC compression molding primarily utilizes high-performance thermosetting resins and fiber-reinforced composites, chosen for their exceptional durability, heat resistance, and flame retardancy. Base resins like Phenolic offer inherent flame resistance and electrical insulation, making them ideal for safety-critical components. Epoxy resins provide superior mechanical strength and chemical resistance for high-pressure parts. Unsaturated Polyester offers a cost-effective solution for general applications. Fiber-reinforced composites like SMC and BMC significantly enhance structural strength, enabling the production of large, lightweight, and robust components that can replace metal, drastically improving design flexibility and product lifespan.
Key Materials: Phenolic • Epoxy • Unsaturated Polyester • SMC • BMC
| Material Type | Properties | Main Applications |
|---|---|---|
| Phenolic Resin (Thermoset) | Princípio do Processo. | Junction boxes, terminal blocks, circuit breaker housings, valve bodies, fan blade skeletons, handles. |
| Epoxy Resin (Thermoset) | Superior mechanical strength and adhesion, very low shrinkage (<0.5%), excellent chemical resistance (to acids, alkalis, refrigerants), good electrical insulation. | High-pressure valve bodies, pump impellers and casings, electronic encapsulations, precision sensor brackets. |
| Unsaturated Polyester Resin (Thermoset) | Good overall mechanical properties, fast curing speed, good processability, moderate cost, easy to color. | Air conditioner panels, decorative grilles, air outlet louvers, housing components. |
| SMC (Sheet Molding Compound) | Extremely high strength-to-weight ratio, excellent dimensional stability, outstanding heat and weather resistance, high design freedom, can form large complex parts. | Outdoor unit casings, large fan impellers, high-strength structural brackets, access panels. |
| BMC (Bulk Molding Compound) | Excellent flowability and filling ability, suitable for complex shapes, large variations in wall thickness, and precision parts with inserts. | Valve bodies with metal inserts, motor mounting bases, complex electronic component housings, automotive AC compressor parts. |
| Special Fiber Reinforced | Extreme lightweight and high rigidity (Carbon Fiber); high impact resistance and wear resistance (Aramid Fiber). | High-efficiency fan impellers (Carbon Fiber); special protective covers (Aramid Fiber). |
What are the Advantages and Disadvantages of Using Plastic Compression Molding in HVAC?
Plastic compression molding in HVAC systems delivers superior material performance, exceptional durability, and cost-effectiveness for large, complex parts. It excels with high-strength, heat-resistant thermoset composites, ideal for robust components like fan blades and valve bodies. However, it presents notable challenges including slower production cycles, limited material recyclability, and the need for post-processing to remove flash. While it enables the creation of structurally integral parts with excellent surface finishes, the process is best suited for high-volume production of "beefy" components where its unique material advantages outweigh the slower throughput and sustainability concerns.
Key Balance: Superior Material Performance vs. Slower Cycle Times & Limited Recyclability
Advantages
Superior Material Performance and Durability
Compression molding is ideal for thermosetting plastics and fiber-reinforced composites, offering exceptional heat resistance (150-180°C), outstanding chemical resistance to refrigerants and oils, and high mechanical strength with excellent creep resistance.
Why it's crucial for HVAC: Components near compressors and condensers are exposed to extreme heat and chemicals. This material stability prevents warping, softening, or failure, ensuring long-term system reliability.
Excellent Cost-Effectiveness for Large, Complex Parts
Once the tool is made, the per-part cost is very low for high-volume production. The process uses a precisely measured charge, minimizing material waste.
Why it's crucial for HVAC: For components produced in tens of thousands (e.g., outdoor unit housings, fan blades), the low unit cost directly translates to higher profit margins and more competitive pricing.
Unmatched Design Flexibility and Structural Integrity
The process easily produces parts with very thick walls and significant variations in wall thickness without creating sink marks. It is also highly effective for insert molding, where metal parts are bonded directly into the plastic.
Why it's crucial for HVAC: This allows for the creation of robust, single-piece structures like fan hubs and motor housings, and creates strong, reliable mounting points and electrical connections, eliminating assembly steps.
Superior Surface Finish and Aesthetic Potential
By using a polished or textured mold cavity, manufacturers can produce parts with a Class-A surface finish or a specific grain pattern directly, without painting.
Why it's crucial for HVAC: For consumer-facing products like indoor unit panels, a high-quality aesthetic finish is critical for brand perception and eliminates the cost and durability issues of painting.
Disadvantages
Slower Production Cycle Times
The process involves heating the material, holding it under pressure while it cures, and then cooling the mold. This entire cycle can take several minutes, whereas injection molding cycles are often measured in seconds.
Why it's a challenge for HVAC: For very small, high-volume parts where throughput is the absolute priority, injection molding may be a more efficient choice. The slower cycle time limits the number of parts produced per hour.
Limited Material Recyclability
The chemical cross-linking that gives thermosets their superior properties is irreversible. Unlike thermoplastics, they cannot be melted down and re-molded, creating waste streams that typically end up in landfills.
Why it's a challenge for HVAC: As regulations around product lifecycle and sustainability become stricter, this is a growing disadvantage. It also means there is less opportunity to reuse material waste internally.
Extensive Post-Processing is Often Required
Excess material, known as "flash," is forced out of the mold parting line during compression. This flash must be manually or automatically trimmed from each part, adding a secondary labor cost and step to the manufacturing process.
Why it's a challenge for HVAC: This additional handling increases labor costs and cycle time. Inconsistent trimming can also affect part fit and final appearance, requiring quality control checks.
Not Suitable for Thin-Walled or High-Precision Tolerance Applications
The material flows under pressure but doesn't have the high shear flow of injection molding. This makes it difficult to fill very thin walls or reproduce extremely fine, intricate details consistently.
Why it's a challenge for HVAC: Components like thin, flexible air deflectors, micro-valves, or parts with very tight tolerances (±0.05mm or less) are better suited to injection molding or precision machining.
What is the Difference Between Compression Molding and Injection Molding?
Compression molding and injection molding represent two distinct approaches to plastic manufacturing, each with unique advantages for HVAC applications. Compression molding excels with thermosetting materials and large, structurally robust components, while injection molding dominates high-volume production of complex thermoplastic parts. Understanding the fundamental differences in process principles, material compatibility, and cost structures is essential for selecting the optimal manufacturing method for your HVAC components.
Key Considerations: Process Principle • Material Compatibility • Cost Structure • Application Suitability
Detailed Comparison: Compression Molding vs. Injection Molding
| Attribute | Compression Molding | Injection Molding |
|---|---|---|
| Process Principle | A sua peça tem paredes finas, detalhes intrincados ou geometrias complexas. Pense em dispositivos médicos, eletrónica de consumo ou conectores complexos. | Material is melted and injected under high pressure into a closed mold cavity. |
| Primary Materials | Thermosetting Plastics (Phenolic, Epoxy), Fiber-Reinforced Composites (SMC, BMC), some Thermoplastics. | Thermoplastics (Polypropylene, ABS, Polycarbonate, Nylon), some Elastomers. |
| Material State | Starts as a solid, putty-like charge or preform. | Starts as solid pellets, which are fully melted into a liquid before injection. |
| Pressure | Relatively low pressure (typically 1,000 - 5,000 psi). The material flows more like a thick paste. | Extremely high pressure (typically 10,000 - 30,000 psi). The material flows like a thin liquid. |
| Tooling (Molds) | Simpler design, lower internal pressures. Can be made from less expensive materials like cast aluminum or mild steel. | Highly complex, must withstand extreme pressures. Requires precision cooling channels and ejector systems. Made from hardened tool steel. |
| Tooling Cost | Lower. Significantly cheaper to design and build a compression mold. | Higher. Injection molds are among the most expensive and complex manufacturing tools. |
| Cycle Time | Slower. Cycles are measured in minutes, as the "cure" time for thermosets is the bottleneck. | Faster. Cycles are measured in seconds, making it ideal for mass production. |
| Part Geometry | Excellent for large parts, thick-walled sections, and simple-to-moderate complexity. Poor for very thin walls. | Excellent for small parts, thin-walled sections, and highly complex, intricate details. Poor for very thick walls (causes sink marks). |
| Waste | Very Low. Uses a pre-measured charge, so there is minimal scrap. Main waste is "flash" that is trimmed off. | Higher. Creates waste with every shot in the form of sprues, runners, and gates (though thermoplastic waste can be reground and recycled). |
| Insert Molding | Excellent. Metal inserts can be easily placed in the mold before the cycle, and the material flows around them under low pressure. | Good, but more complex. Inserts must be securely held in place against high injection pressure, which can sometimes dislodge them. |
Key Differences & Process Selection Guide
Material Kingdom
- ✓ Compression molding is the king of thermosets and composites
- ✓ Injection molding is the king of thermoplastics
Speed & Volume
- ✓ Injection molding is built for speed and high volume
- ✓ Compression molding is a slower process, better suited for robust, lower-volume, high-value parts
Design Focus
- ✓ Compression molding excels at strong, thick, and large parts
- ✓ Injection molding excels at complex, thin, and detailed parts
Cost Structure
- ✓ Compression molding has low tooling costs but a higher per-part cost
- ✓ Injection molding has high tooling costs but a very low per-part cost at scale
When to Choose Which Process? A Practical Guide
Choose Compression Molding When:
- ✓ Your material is a thermoset plastic or a fiber-reinforced composite (SMC/BMC). This is the number one reason. If you need the heat resistance, chemical resistance, or strength of these materials, compression molding is your primary choice.
- ✓ Your part is large, thick-walled, or requires high structural strength. Think car hoods, large electrical housings, or robust HVAC fan blades.
- ✓ You need to incorporate metal inserts. The low-pressure flow is gentler and more reliable for encapsulating inserts.
- ✓ Your production volume is moderate, and you need to minimize upfront tooling investment.
Choose Injection Molding When:
- ✓ Your material is a thermoplastic. This is its domain.
- ✓ You need to produce millions of parts at the lowest possible unit cost. The speed of injection molding is unbeatable for mass production.
- ✓ Your part has thin walls, intricate details, or complex geometries. Think medical devices, consumer electronics, or complex connectors.
- ✓ O composto termoendurecível utilizado, como o Composto de Moldagem em Folha (SMC) ou o Composto de Moldagem em Massa (BMC). O custo varia consoante o tipo de carga (fibra de vidro), resina e aditivos.
- ✓ Material recyclability is a key part of your sustainability strategy.
How is Quality Controlled and Inspected in the HVAC Compression Molding Process?
Quality control in HVAC compression molding is a comprehensive process that spans from pre-production to post-production stages. It involves rigorous material testing, tool validation, real-time process monitoring, and thorough inspection of finished components. By implementing advanced inspection technologies like CMMs, ultrasonic testing, and thermography, manufacturers ensure that HVAC components meet precise dimensional tolerances, structural integrity requirements, and performance standards. This systematic approach to quality control results in reliable, durable parts that can withstand the demanding conditions of HVAC systems.
Key Quality Stages: Pre-Production Control • In-Process Monitoring • Post-Production Inspection • Advanced Testing Methods
Pre-Production Quality Control
Material Inspection
Raw materials (e.g., SMC, BMC) undergo viscosity, fiber content, and thermal performance testing to ensure compliance with specifications.
Tooling Inspection
Molds are examined for dimensional accuracy, surface finish, and wear using technologies like Coordinate Measuring Machines (CMM).
Process Parameter Validation
Heating temperature, pressure, and curing time are validated to ensure optimal material flow and curing.
In-Process Quality Control
Process Testing
Sensors and data acquisition systems continuously monitor parameters such as mold temperature, pressure, and curing time.
Visual Inspection
Operators check for immediate defects such as flash, short shots, or discoloration during the molding process.
Cure Monitoring
Thermography and ultrasonic technologies monitor the curing process to ensure complete cross-linking of thermosetting materials.
Post-Production Quality Control
Dimensional Inspection
CMMs and optical scanners measure part dimensions against CAD models to ensure tolerance requirements are met.
Mechanical Testing
Tests for tensile strength, impact resistance, and hardness are performed to validate structural integrity.
Surface Finish Evaluation
Parts are inspected for surface defects, with additional finishing processes (e.g., sanding, painting) applied if needed.
Functional Testing
For HVAC-specific components, tests may include thermal cycling, pressure resistance, and airflow performance.
Inspection Methods and Technologies
Dimensional Inspection
- • Coordinate Measuring Machines (CMM): High-precision measurements of complex geometries
- • 3D Scanning: Captures detailed surface data for comparison with design models
Material & Structural Inspection
- • Ultrasonic Testing: Detects internal defects such as voids or delamination
- • Thermography: Monitors temperature distribution during curing
Surface & Visual Inspection
- • Visual Inspection: Trained operators identify surface defects like cracks, flash, or discoloration
- • Automated Vision Systems: Use cameras and AI to automatically detect surface defects
Quality Control Standards and Certifications
Adherence to industry standards and certifications ensures consistency and reliability in compression molding processes. Key standards include:
ISO 9001
The widely recognized international standard for Quality Management Systems (QMS), ensuring that products and services consistently meet customer and regulatory requirements. It demonstrates a commitment to quality and continuous improvement.
ISO 13485
Specifies requirements for a comprehensive QMS for the design and manufacture of medical devices. While specific to the medical industry, its principles of risk management and traceability are often applied to high-reliability HVAC components.
ISO 14001
The standard for Environmental Management Systems (EMS), helping organizations minimize their environmental impact, reduce waste, and ensure compliance with environmental regulations. It reflects a commitment to sustainable manufacturing practices.
ISO 45001
The international standard for Occupational Health and Safety Management Systems (OHSMS), providing a framework to improve employee safety, reduce workplace risks, and create safer working conditions in manufacturing environments.
How Much does Compression Molding Cost?
The cost of compression molding is highly variable, influenced by a combination of one-time tooling expenses and per-unit production costs. For HVAC components, total costs can range from a few dollars for simple, high-volume parts to hundreds of dollars for complex, low-volume items. The primary cost drivers include mold complexity (ranging from $1,000 to over $100,000), raw material selection (SMC/BMC typically $1.50-$10.00 per pound), production volume (which critically amortizes tooling costs), and the required cycle time. Unlike injection molding, compression molding offers lower tooling costs, making it economically viable for medium-volume production runs (typically 1,000 to 100,000 units), a common requirement for specialized HVAC enclosures, housings, and structural components.
Key Cost Components: Mold Tooling • Raw Materials • Machine Time & Labor • Post-Processing • Volume Amortization
Detailed Cost Breakdown
| Cost Component | Description | Estimated Range & Factors |
|---|---|---|
|
Mold Tooling (One-Time)
|
Design and fabrication of the compression mold. Includes cavity number, material (steel/aluminum), surface finish, and complexity (undercuts, side-actions).
|
$1,000 - $100,000+
Low: Simple, single-cavity aluminum mold. High: Multi-cavity, hardened steel mold with tight tolerances and texture for complex HVAC housing. |
|
Raw Materials (Per Unit)
|
The thermoset compound used, such as Sheet Molding Compound (SMC) or Bulk Molding Compound (BMC). Cost varies with filler type (glass fiber), resin, and additives.
|
Preocupação do cliente: Ciclo de produção e eficiência, afetando o planeamento do projeto e os custos
Cost is calculated per part based on part weight and material density. High-performance, flame-retardant BMC for HVAC will be at the higher end. |
|
Machine & Labor (Per Unit)
|
Cost of the compression press cycle time, energy consumption, and operator/technician oversight. Highly automated processes reduce labor costs.
|
$0.10 - $5.00 per part
Depends on cycle time (30 seconds to 5+ minutes) and level of automation. Larger, thicker parts have longer cycles and higher costs. |
|
Post-Processing (Per Unit)
|
Operations required after molding, such as trimming flash, drilling holes, machining surfaces, painting, or adding inserts.
|
$0.05 - $2.00+ per part
Simple manual trimming is low cost. CNC machining, painting, or assembly of multiple parts significantly increases this cost. |
|
Overhead & Quality (Per Unit)
|
Indirect costs including quality inspection, maintenance, administrative costs, and profit margin.
|
~10-20% of total cost
This is a percentage applied to the sum of the other costs. Strict HVAC quality standards (e.g., for flame retardancy) can increase this. |
Key Factors Influencing Cost
Production Volume
This is the most critical factor. High volumes dramatically lower the per-unit cost by amortizing the one-time mold tooling expense over a larger number of parts. Compression molding is ideal for medium volumes where injection molding tooling is prohibitively expensive.
Mold Complexity & Cavities
A simple, single-cavity mold is the cheapest. Costs increase with complex geometries, tight tolerances, textured surfaces, and the number of cavities. A multi-cavity mold has a higher upfront cost but a much lower per-part cost for high-volume runs.
Part Size & Thickness
Larger parts require more material, larger and more expensive molds, and larger compression presses. Thicker sections also increase cycle time (as they take longer to heat and cool), directly increasing machine and labor costs per part.
Material Selection
Standard SMC is cost-effective. Costs rise for specialized BMC compounds with high glass fiber content, flame retardants (critical for HVAC), UV stabilizers, or other performance-enhancing additives required for demanding applications.
Frequently Asked Questions
Our compression molding FAQ addresses key customer concerns including prototype validation, insert molding, material selection, production cycles, post-processing, minimum order quantities, common defect avoidance, and supplier selection. We offer soft mold prototype production, 3D printing and CNC machining verification, material testing services, support metal insert molding, and recommend the most suitable materials based on application environments (such as phenolic resins, epoxy resins, SMC, BMC, etc.). Production cycles typically range from 1-5 minutes, we provide various post-processing services and maintain flexible MOQ policies. We strictly control common defects in the production process and provide comprehensive supplier evaluation criteria to ensure customers receive high-quality HVAC compression molding solutions.
Key Services: Prototype Validation • Insert Molding • Material Selection • Post-processing • Quality Control
How to Validate HVAC Compression Molding Parts Before Making Formal Molds?
Customer concern: How to verify design feasibility before investing in expensive mold costs
+
How to Validate HVAC Compression Molding Parts Before Making Formal Molds?
Customer concern: How to verify design feasibility before investing in expensive mold costs
Our Solutions:
Soft Mold Prototype Production:
Using lower-cost materials (such as aluminum alloy or epoxy resin) to make molds for small batch (tens to hundreds of pieces) production validation. This can test dimensional accuracy, assembly relationships, material performance, and performance under actual operating conditions.
3D Printing and CNC Machining:
For complex shapes or structures requiring rapid validation, physical models can be created through 3D printing or CNC machining for assembly and functional testing. Although this cannot fully simulate the physical properties of compression materials, it can quickly verify design structure.
Material Testing:
Directly using target materials (such as BMC or SMC) to make test strips in standard test molds for mechanical properties (such as tensile strength, impact strength), thermal properties (such as heat deflection temperature), and electrical performance testing to ensure materials meet specific HVAC application requirements.
Does Compression Molding Support Metal Inserts or Other Material Inserts?
Customer concern: Whether other material components can be integrated during the compression molding process
+
Does Compression Molding Support Metal Inserts or Other Material Inserts?
Customer concern: Whether other material components can be integrated during the compression molding process
Our Solutions:
Yes, compression molding is very suitable for insert molding. Before placing plastic materials (premixed compounds or preformed sheets) into the mold, metal inserts (such as threaded nuts, terminals, sensor probes, etc.) or other materials (such as another molded plastic part) can be precisely placed at predetermined positions in the mold. When the mold is closed and pressure is applied, the molten plastic material will flow and wrap around the inserts, forming a strong integral whole after cooling and curing.
Advantages:
This process greatly simplifies subsequent assembly steps, improves structural strength and reliability of components, reduces total production costs, and is widely used in HVAC electrical components and connectors.
How to Select the Most Suitable Compression Molding Material for Specific HVAC Applications?
Customer concern: How to select appropriate materials based on application environment, performance requirements, and cost factors
+
How to Select the Most Suitable Compression Molding Material for Specific HVAC Applications?
Customer concern: How to select appropriate materials based on application environment, performance requirements, and cost factors
Our Material Selection Guide:
High-temperature environments (such as near engines or heating elements):
Prioritize phenolic resins or epoxy resins, which have excellent thermal stability and dimensional stability.Applications requiring high mechanical strength and impact resistance (such as fan housings, brackets):
Select fiber-reinforced composite materials, such as SMC (Sheet Molding Compound) or BMC (Bulk Molding Compound). The content and length of glass fibers directly affect their strength. SMC is typically used for larger, flatter parts, while BMC is more suitable for small parts with complex shapes.Electrical insulation applications (such as junction boxes, switch housings):
Phenolic resins and urea-formaldehyde resins are ideal choices due to their excellent electrical insulation and flame retardancy.Chemical corrosion resistance (such as exposure to refrigerants or cleaning agents):
Polyester resins and epoxy resins provide good chemical corrosion resistance.Cost-sensitive applications:
Polyester resins are typically the most cost-effective option, especially when performance requirements are not extremely demanding.
What is the Typical Production Cycle for HVAC Compression Molding? What are the Key Factors Affecting Efficiency?
Customer concern: Production cycle and efficiency, affecting project planning and costs
+
What is the Typical Production Cycle for HVAC Compression Molding? What are the Key Factors Affecting Efficiency?
Customer concern: Production cycle and efficiency, affecting project planning and costs
O fornecedor tem capacidades de serviço de processo completo desde a otimização do design do produto (DFM, Design for Manufacturability) até ao desenvolvimento de moldes? Podem intervir antecipadamente para ajudar a otimizar o seu design, reduzindo custos e melhorando o desempenho?
Compared to injection molding, compression molding cycles are typically longer, generally between 1 to 5 minutes, depending on the part size, thickness, and material type.
Material Curing Time:
Thermosetting materials require sufficient time to complete cross-linking reactions (curing) within the mold, which is the most time-consuming part of the cycle. The greater the thickness, the longer the curing time.Mold Temperature:
The mold needs to be heated to a specific temperature to initiate the curing reaction, and after molding, it needs to be cooled to a certain temperature before opening. Efficient temperature control systems can shorten heating and cooling times.Part Geometry and Wall Thickness:
Complex shapes and overly thick cross-sections increase the difficulty of material flow and curing, thereby extending the cycle.Degree of Automation:
Although compression molding is often considered semi-automatic, adopting automation measures such as automatic feeding and robotic part removal can significantly reduce auxiliary time and improve overall production efficiency.
What Post-processing Can Be Performed on Compression Molded HVAC Components?
Customer concern: Post-molding processing to meet final product functional and appearance requirements
+
What Post-processing Can Be Performed on Compression Molded HVAC Components?
Customer concern: Post-molding processing to meet final product functional and appearance requirements
Our Post-processing Services:
Mechanical Processing:
Due to the limited precision of compression molded parts, secondary processing such as CNC milling, drilling, and tapping is often required for holes, slots, or mounting surfaces that require high-precision fitting.
Deburring/Flash Removal:
Removing excess material (flash) generated at the mold parting line to make the appearance neater.
Surface Treatment:
Spray Painting/Coating: Providing color, enhancing weather resistance (UV resistance) or corrosion resistance.
Silk Screen/Pad Printing: Used for adding brand logos, model identifications, or functional instructions.
Texture Treatment: Mold surfaces can be pre-textured (such as leather grain, matte) to give parts a more textured feel and hide minor defects.
Assembly:
Assembling molded parts with other components (such as metal brackets, sealing strips, electronic components) into final products.
Does Compression Molding Service Have Minimum Order Quantity (MOQ) Requirements?
Customer concern: Minimum order quantity, especially for small batch trial production or startup projects
+
Does Compression Molding Service Have Minimum Order Quantity (MOQ) Requirements?
Customer concern: Minimum order quantity, especially for small batch trial production or startup projects
Our MOQ Policy:
This typically depends on the supplier and specific project circumstances. Due to the relatively low mold costs of compression molding, its MOQ is usually much lower than injection molding.
For Standard Products:
Suppliers may set a reasonable MOQ (such as several hundred pieces) to balance production preparation costs.
For Custom Projects:
MOQ is more flexible. In the early stages of a project, suppliers may be willing to accept smaller order quantities (such as tens of pieces) for prototype validation or small batch trial production. As the project enters mass production, MOQ will increase accordingly to achieve economies of scale.
Recommendation:
Clearly communicate your expected production volume and order plans with suppliers in the early stages of the project to obtain the most suitable cooperation plan.
What are the Common Defects in Compression Molding? How to Avoid Them?
Customer concern: Product quality control and solutions to common problems
+
What are the Common Defects in Compression Molding? How to Avoid Them?
Customer concern: Product quality control and solutions to common problems
Common Defects and Solutions:
Short Shot/Incomplete Filling:
Causes: Insufficient material quantity, poor material flow, inadequate mold temperature or pressure.
Avoidance Methods: Precisely weigh materials, preheat materials, increase mold temperature or holding pressure.
Bubbles/Voids:
Causes: Moisture or volatiles in materials, too fast curing speed, insufficient pressure causing gas to be unable to escape.
Avoidance Methods: Fully dry materials, adjust curing speed, adopt appropriate pressure curves.
Warpage:
Causes: Uneven cooling, inconsistent material shrinkage, improper ejection system design.
Avoidance Methods: Optimize mold cooling system, adjust holding time and pressure, improve ejection design.
Excessive Flash:
Causes: Excessive material placement, insufficient clamping force, worn or poorly fitting mold parting surfaces.
Avoidance Methods: Precisely control material quantity, increase clamping force, repair or maintain molds.
What Capabilities Should Be Key Considerations When Selecting HVAC Compression Molding Suppliers?
Customer concern: How to select reliable suppliers to ensure product quality and delivery capability
+
What Capabilities Should Be Key Considerations When Selecting HVAC Compression Molding Suppliers?
Customer concern: How to select reliable suppliers to ensure product quality and delivery capability
Key Supplier Evaluation Capabilities:
Engineering and Design Capabilities:
Does the supplier have full-process service capabilities from product design optimization (DFM, Design for Manufacturability) to mold development? Can they intervene early to help optimize your design to reduce costs and improve performance?Moldagem por Compressão para Componentes de AVAC | HVACore
Is the supplier familiar with the characteristics of various HVAC thermosetting materials (BMC, SMC, phenolic, etc.) and can recommend the most suitable materials based on your needs?Quality Control Systems:
Has the supplier passed ISO or other quality system certifications? Do they have comprehensive testing equipment (such as CMM coordinate measuring machines) and processes to ensure consistency of dimensional accuracy and material properties?Production Equipment and Automation Level:
The tonnage, precision, and automation level of equipment directly determine production efficiency and product quality stability.Value-added Services and Certifications:
Can they provide one-stop services such as rapid prototyping, assembly, surface treatment, and product certification testing (such as UL, CE, etc.)? This can significantly shorten your product time-to-market.Let's Start Your Compression Molding Project
Partner with HVACore for precision compression molding solutions. Our expert team is ready to transform your HVAC component requirements into high-quality manufactured parts.