
ABS ou HIPS
– The indoor unit housing, front panel, louver blades, and air filter frame are all injection-molded plastic components that directly affect performance and longevity
– ASA (Acrylonitrile Styrene Acrylate) is the material of choice for outdoor unit housings due to its superior UV resistance and weatherability compared to standard ABS
– Achieving flat, warp-free large plastic panels at scale is the single biggest manufacturing challenge in ductless mini split production
– Modern mini split plastic components are designed with snap-fit assemblies and ultrasonic welding joints that allow tool-free field disassembly for maintenance
What Is a Ductless Mini Split System?
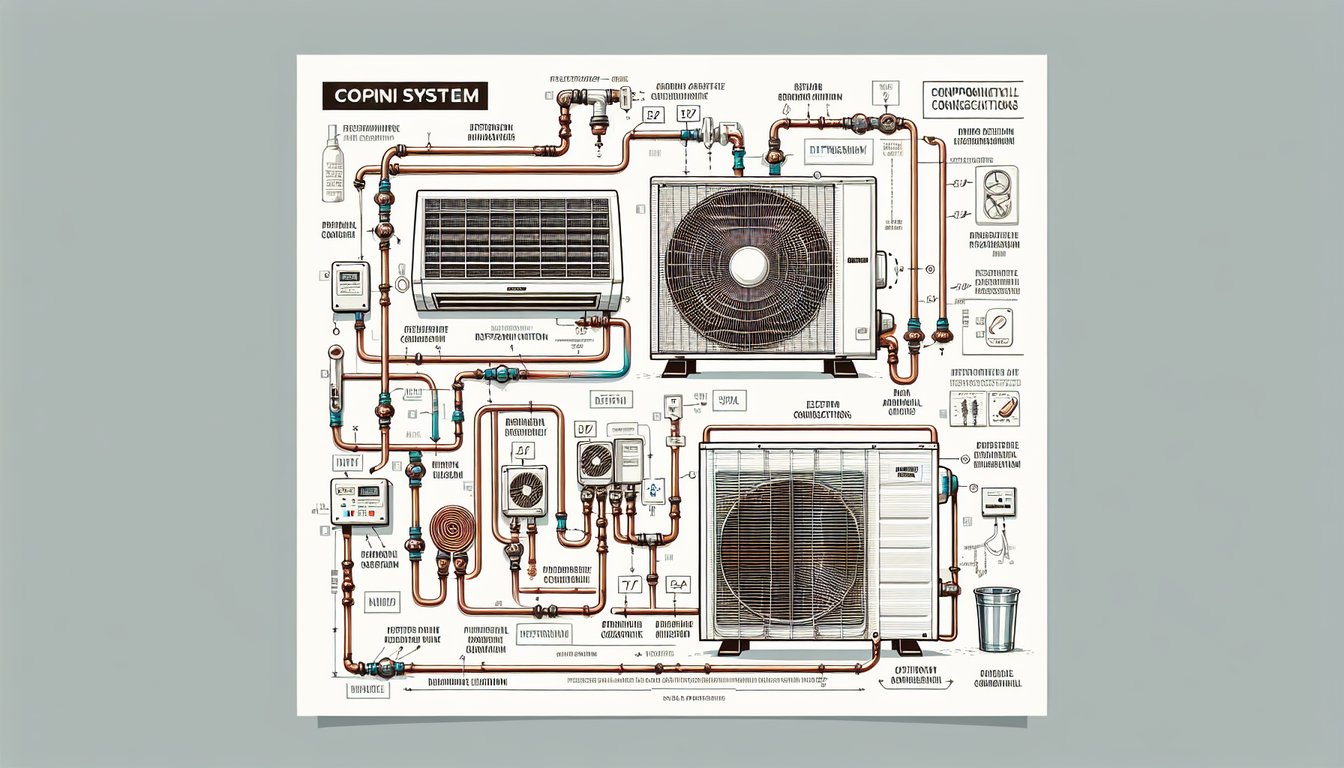
A ductless mini split is a zoned heating and cooling system that transfers thermal energy between a wall-mounted indoor air handler and an outdoor compressor/condenser unit via a set of refrigerant lines, a power cable, and a condensate drain line. Unlike central forced-air systems, it requires no ductwork, which is exactly where the “ductless” name comes from.
In our HVAC production facility, we’ve been manufacturing plastic components for ductless mini split systems for over a decade. What strikes us most is how deceptively complex these compact units are. Each mini split system typically consists of:
- Indoor air handler (evaporator unit) — mounted high on an interior wall, it draws room air across a refrigerant coil, then re-circulates conditioned air
- Outdoor condenser unit — houses the compressor, condenser coil, and expansion valve; rejects or absorbs heat from ambient air
- Refrigerant line set — copper tubing carrying refrigerant between the two units, typically pre-insulated and routed through a small wall penetration
The market for ductless mini splits has grown explosively. The U.S. alone installed over 14 million units in 2025, driven by energy efficiency mandates, housing retrofits, and SEER1 requirements that reward zone-by-zone control. From a manufacturer’s standpoint, this growth means plastic component quality has never mattered more — every housing, panel, and louver blade must perform reliably for 10–20 years across extreme temperature swings.
True
Multi-zone ductless mini split systems use one outdoor unit connected to multiple indoor air handlers, each independently controlled. This allows heating one zone while cooling another — a genuine capability enabled by variable-speed inverter compressors and zone-specific refrigerant flow management.
False
Modern multi-zone ductless systems can condition entire homes or commercial spaces. A single outdoor unit can support up to 8 indoor air handlers covering over 3,000 sq ft. The “mini” refers to the compact, duct-free design — not a limitation on total capacity or coverage area.
What Are the Key Plastic Components in a Ductless Mini Split?
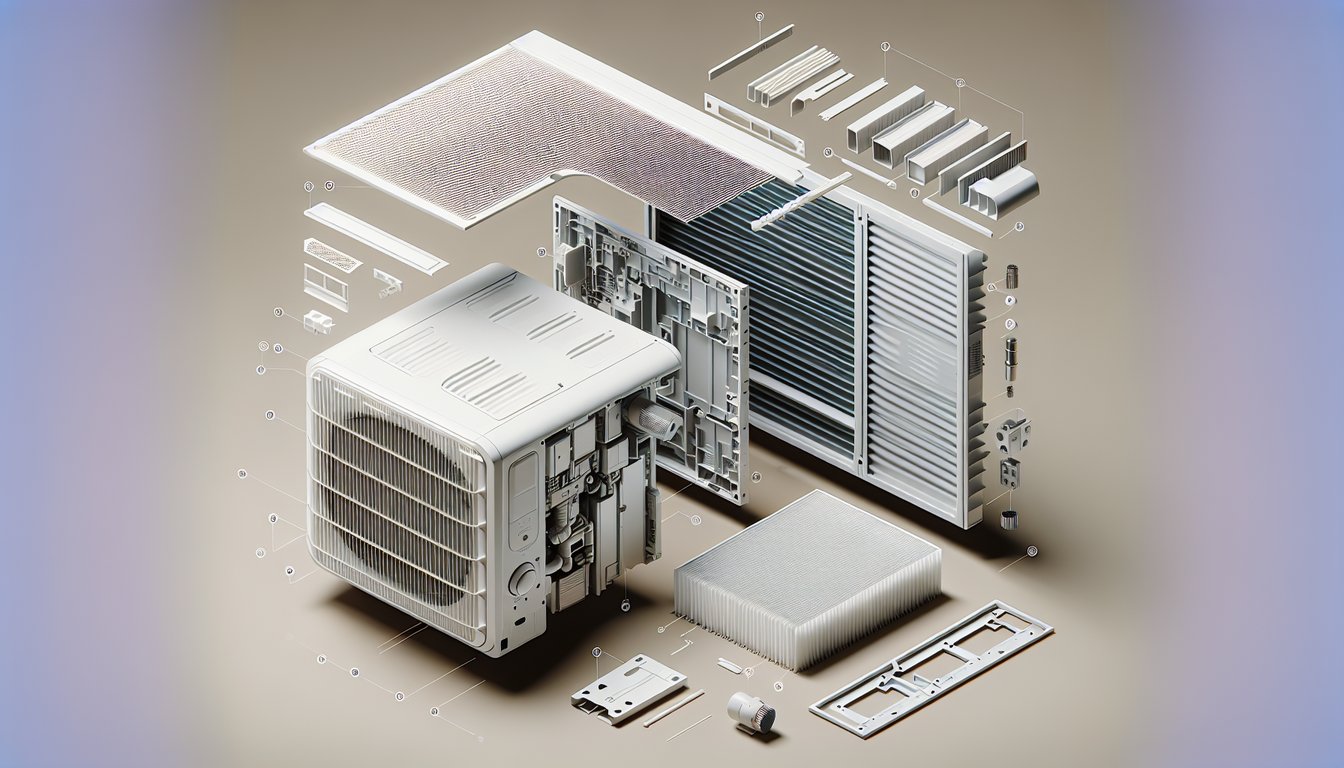
When we break down a typical ductless mini split indoor unit, we count between 12 and 18 discrete injection-molded plastic parts, each with its own material specification and dimensional tolerance. Here’s how we categorize them:
| Component | Typical Material | Critical Requirement | Typical Wall Thickness |
|---|---|---|---|
| Front panel / fascia | ABS or ABS/PC blend | Surface finish, dimensional stability | 2.0–2.5 mm |
| Horizontal louver blades | ABS | Flex fatigue life >50,000 cycles | 1.2–1.8 mm |
| Vertical vanes | ABS | Dimensional accuracy ±0.15 mm | 1.0–1.5 mm |
| Air filter frame | ABS or PP | Filter retention, easy removal | 1.5–2.0 mm |
| Drain pan | PP or ABS | Leak-free, mold-resistant surface | 2.5–3.0 mm |
| Blower housing | ABS or HIPS | Fase de injeção | 2.0–3.0 mm |
| Mounting plate / back plate | ABS or PP-GF | Load-bearing, screw pull-out strength | 3.0–4.0 mm |
| Outdoor housing panels | ASA | UV resistance, impact strength in cold | 2.5–3.5 mm |
| Outdoor condenser grille | ASA or ASA/PC | Airflow-optimized, anti-corrosion | 1.5–2.0 mm |
We’ve found that the front fascia panel is the single component that generates the most customer complaints — hairline sink marks, uneven surface gloss, or post-weld warpage are all visible immediately. Getting this part right requires careful gate location selection, balanced runner design, and holding pressure profiles tuned down to the millisecond.
Which Plastic Materials Are Best for Mini Split Housings?
Material selection is one of the most consequential decisions in mini split housing design. In our experience, the choice comes down to application zone — indoor versus outdoor — and the specific stress profile each part faces.
For indoor units: ABS (Acrylonitrile Butadiene Styrene) remains the workhorse material. Its excellent surface finish capability, ease of painting, and balanced impact/stiffness profile make it ideal for fascia panels, louver blades, and filter frames. An ABS/PC (polycarbonate) blend is often specified for the front panel when the client wants improved impact resistance and a higher-quality feel at a modest cost premium.
For outdoor units: ASA (Acrylonitrile Styrene Acrylate)2 is the definitive choice. ASA’s acrylic-based weathering resistance gives it dramatically better performance than ABS under prolonged UV exposure — we’ve measured ΔE color shift values of 8.0 for standard ABS after 2,000 hours of Xenon arc weathering. In climates like Arizona or Florida, this difference translates directly to whether an outdoor housing looks acceptable at year 5 or has turned chalky yellow.
Key material comparison for outdoor mini split housings:
| Property | ABS | ASA | ASA/PC Blend |
|---|---|---|---|
| UV resistance | Poor (yellows quickly) | Excellent | Excellent |
| Impact strength at -20°C | Moderate | Good | Excellent |
| Heat deflection temp | ~88°C | ~90°C | ~100°C |
| Surface finish quality | Excellent | Very Good | Very Good |
| Relative material cost | 1.0× | 1.3× | 1.6× |
| Processing ease | Easy | Easy | Moderate |
We also specify flame-retardant ABS grades meeting UL 94 V-0 for any components adjacent to electrical wiring — this includes the control board enclosure and wiring harness clips inside the indoor unit. Flame retardant additives do affect surface aesthetics slightly, so we typically apply a texture pattern on these components to mask any flow lines.
True
ASA (Acrylonitrile Styrene Acrylate) is specifically engineered for outdoor UV resistance. Unlike ABS, which yellows and becomes brittle within 2–3 years of direct sun exposure, ASA retains tensile strength and color stability for 10+ years — making it the preferred resin for mini split outdoor unit housings.
False
UV stabilizer additives extend ABS outdoor life from ~2 years to 4–5 years, but they cannot replicate ASA’s inherent acrylate rubber backbone that provides intrinsic weathering resistance. Leading HVAC manufacturers (Daikin, Mitsubishi Electric) specify ASA for outdoor housings precisely because UV-stabilized ABS still degrades measurably faster under continuous solar and thermal cycling.
How Does Injection Molding Shape Ductless Mini Split Components?
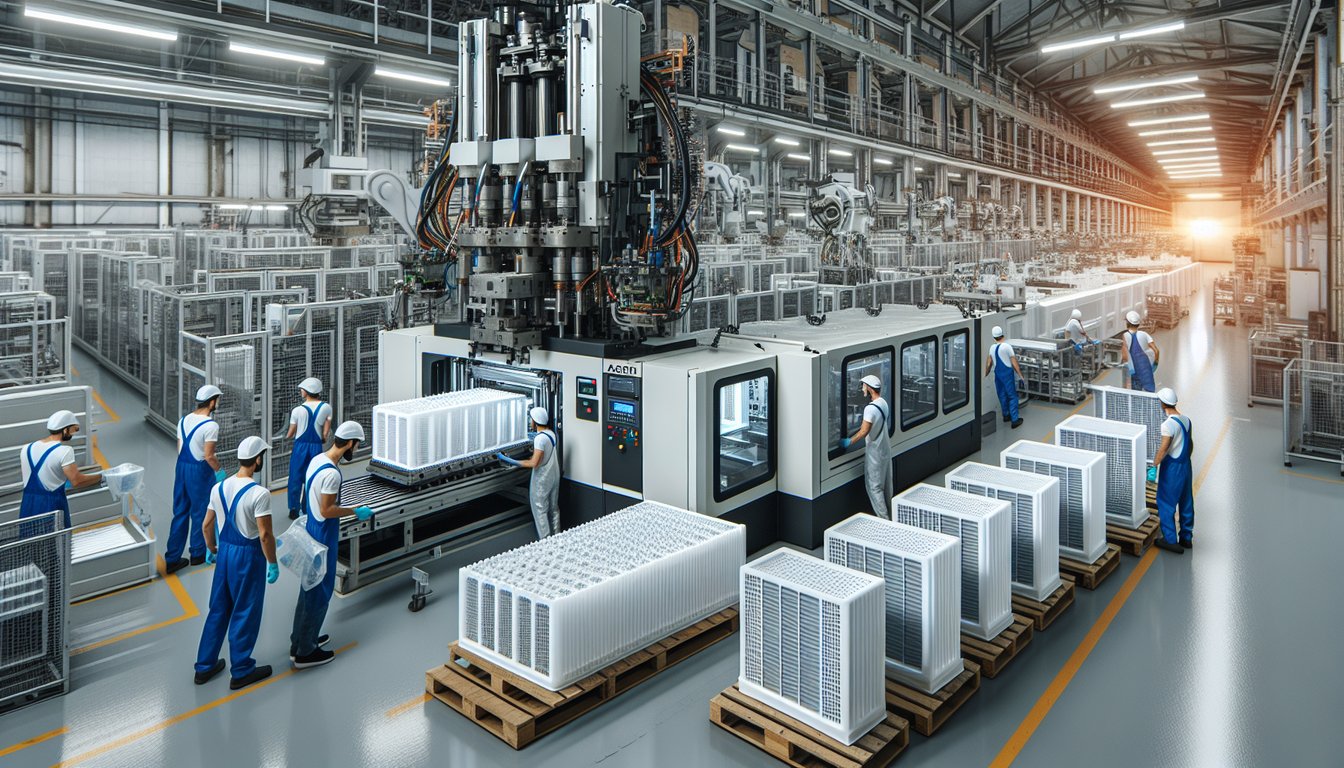
Injection molding3 is the dominant manufacturing process for ductless mini split plastic parts because it delivers the tight dimensional tolerances, high surface quality, and cost-per-part economics that HVAC OEMs demand at scale.
Here’s how our injection molding process works for a typical mini split front fascia panel:
- Mold design and DFM review — Before cutting steel, we run mold flow analysis simulations to predict fill patterns, weld line locations, and warpage. For a 600 mm × 250 mm front panel, we typically use a 3-gate hot runner system to balance fill and minimize weld lines in visible areas.
- Material drying — ABS and ASA are hygroscopic; moisture above 0.05% causes silver streaks and splay on the surface. We dry all materials to <0.02% moisture content in desiccant hoppers before processing.
- Injection phase : Em regiões de elevada radiação UV (Zona de Resistência de Plantas USDA 9+), as superfícies plásticas exteriores podem receber doses cumulativas de UV equivalentes a mais de 4.000 horas de exposição a arco de xenónio ao longo de um ciclo de vida de 10 anos. Para o ABS, isto degrada progressivamente a fase de borracha de polibutadieno, causando empolamento superficial, aumento da fragilidade e alteração da cor. O ASA resiste a este mecanismo porque o seu componente acrílico de borracha absorve a radiação UV sem degradação fotolítica.
- Packing and holding — Holding pressure (typically 60–75% of peak injection pressure) is applied for 8–15 seconds to pack out sink marks before the gate freezes. This is where wall thickness uniformity becomes critical.
- Cooling — Mold temperature of 50–65°C provides the right balance between surface quality and cycle time. Conformal cooling channels in our newer tooling reduce cooling time by 20–30% versus conventional drilled channels.
- Ejection and post-processing — Parts are ejected using a combination of ejector pins and air assist. Large panels require careful ejection to avoid deformation while still warm.
| Component | Material | Function |
|---|---|---|
| Outdoor unit housing | ASA | UV and weather resistance |
| Indoor unit front panel | ABS/PC blend | Aesthetic finish, impact resistance |
| Refrigerant line cover | ASA | Long-term UV stability |
| Drain pan | PP | Chemical resistance, moisture tolerance |
Clamping tonnage for the largest mini split panels typically requires 400–800 tonne presses. We run 24/7 production cycles with automated part removal via 6-axis robot, targeting cycle times of 45–65 seconds per shot.
What Are the Biggest Manufacturing Challenges for Mini Split Plastic Parts?
In our experience, ductless mini split plastic production presents a unique set of manufacturing challenges that differ from typical injection molding work. These are the five issues we deal with most frequently:
Challenge 1: Warpage in large flat panels
| Specification | Value |
|---|---|
| Housing wall thickness | 2.5–3.5 mm |
| Draft angle (standard) | 1.5–2° |
| Surface finish | SPI A2 (gloss) / MT-11050 (texture) |
| Dimensional tolerance | ±0.2 mm on fit features |
The front fascia panel of a mini split indoor unit is essentially a large, thin, flat part — the worst-case scenario for warpage. Differential cooling across the part’s surface creates asymmetric residual stresses that manifest as bow, twist, or saddle distortion after ejection. We control this through balanced cooling channel design, consistent wall thickness (eliminating abrupt thickness changes), and careful gate placement to ensure uni-directional fill.
Challenge 2: Sink marks at reinforcing ribs
To stiffen the front panel without adding wall thickness, designers add ribs on the back surface. However, material behind these ribs cools more slowly, creating depressions (sink marks) visible on the Class-A front surface. Our rule of thumb: rib thickness should not exceed 50–60% of the nominal wall thickness. For our standard 2.2 mm ABS panel, ribs are kept at 1.1–1.3 mm maximum.
Challenge 3: Louver blade flex fatigue
Horizontal louver blades in mini split units cycle open and closed thousands of times per year. At ±45° swing amplitude, the living hinge or pivot mechanism accumulates fatigue stress. We design pivot points with generous radius transitions (minimum 0.5 mm) and use ABS grades with higher rubber content for improved flex endurance.
| Specification | Value |
|---|---|
| Housing wall thickness | 2.5–3.5 mm |
| Draft angle (standard) | 1.5–2° |
| Surface finish | SPI A2 (gloss) / MT-11050 (texture) |
| Dimensional tolerance | ±0.2 mm on fit features |
Challenge 4: Weld lines in structural components
When two flow fronts meet in a mold cavity, they form a weld line — a structurally weaker zone. For the outdoor condenser grille, which must withstand accidental impact, we use mold flow analysis to push weld lines to non-critical areas, and we post-mold test grille impact resistance to UL 1995 standards.
Challenge 5: Color matching across multi-part assemblies
A mini split unit can have 6–8 white plastic components that must visually match. Batch-to-batch colorant variation, process-induced surface gloss differences, and UV aging rates all create matching challenges. We address this with tight lot-based material certification and a 45° gloss spectrometer check on every production lot.
How Do Weather and UV Exposure Affect Mini Split Outdoor Unit Plastics?
| ASA vs ABS | ASA | ABS |
|---|---|---|
| UV resistance | Excellent (10+ yr) | Poor (2–3 yr) |
| Color stability | ΔE <3 / 1000h xenon | ΔE >10 / 500h |
| Impact strength | High | High |
| Cost premium | +30% | Baseline |
| Material | UV Resistance | Impact Strength | Cost Index |
|---|---|---|---|
| ASA | Excellent (10+ yr) | High | 1.3× |
| ABS | Poor (2–3 yr) | High | 1.0× |
| UV-stabilized ABS | Moderate (4–5 yr) | High | 1.15× |
| PP | Moderate | Medium | 0.85× |
| Process Stage | Parameter | Typical Range |
|---|---|---|
| Injection | Melt temperature (ASA) | 230–250°C |
| Packing | Holding pressure | 60–80% of injection pressure |
| Cooling | Mold temperature | 50–70°C |
| Ejection | Cycle time | 30–60 s (housing panels) |
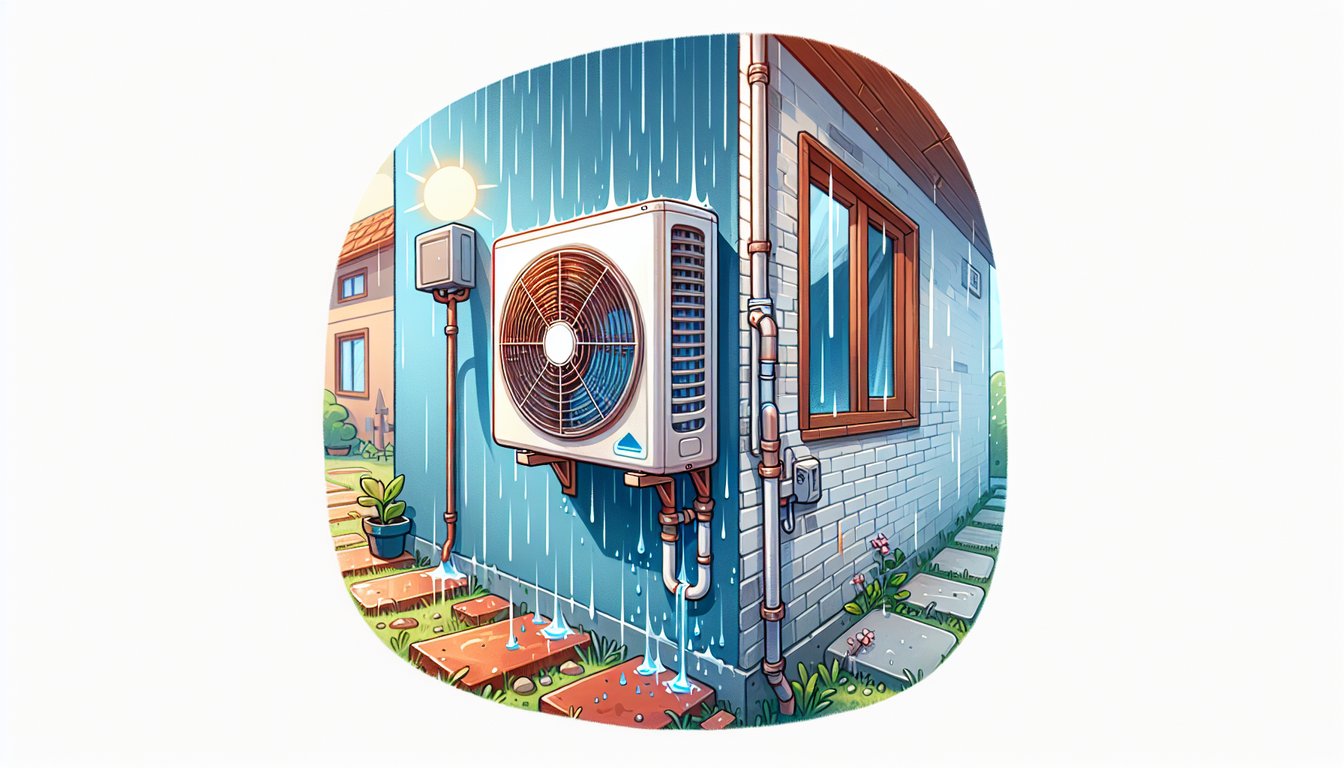
The outdoor unit of a ductless mini split endures conditions that would destroy most consumer plastic products within a few years. In our HVAC production facility, we test outdoor housing panels against a battery of environmental stressors before approving any material specification change.
UV Radiation
| Specification | Value |
|---|---|
| Housing wall thickness | 2.5–3.5 mm |
| Draft angle (standard) | 1.5–2° |
| Surface finish | SPI A2 (gloss) / MT-11050 (texture) |
| Dimensional tolerance | ±0.2 mm on fit features |
: In high-UV regions (USDA Plant Hardiness Zone 9+), outdoor plastic surfaces can receive cumulative UV doses equivalent to 4,000+ hours of Xenon arc exposure over a 10-year lifespan. For ABS, this progressively degrades the polybutadiene rubber phase, causing surface chalking, increased brittleness, and color shift. ASA resists this mechanism because its acrylic rubber component absorbs UV without photolytic degradation.
ASTM D4329: Outdoor units in continental climates can see temperature swings from -30°C in winter to +65°C surface temperature in direct summer sun. Over 20 years, this represents tens of thousands of thermal cycles, driving dimensional fatigue in snap-fit joints and mounting holes. We design outdoor panels with 0.1–0.2% dimensional clearance allowance for thermal expansion, using the material’s CTE (coefficient of thermal expansion) of ~70 µm/m·°C for ASA.
Rain and Moisture
| Specification | Value |
|---|---|
| Housing wall thickness | 2.5–3.5 mm |
| Draft angle (standard) | 1.5–2° |
| Surface finish | SPI A2 (gloss) / MT-11050 (texture) |
| Dimensional tolerance | ±0.2 mm on fit features |
: While ABS and ASA are not highly moisture-absorbent, prolonged water exposure at joints and fastener penetrations can cause surface staining and promote microbial growth. We specify hydrophobic surface treatments and drainage geometry in outdoor housing design to direct water away from structural features.
Hail and Impact: Mini split outdoor units must be robust against hail strikes up to ANSI/FM 4473 Class 3 severity (1-inch diameter hail at 88 mph). ASA/PC blends offer improved cold-temperature impact resistance versus plain ASA, and we recommend them for installations in hail-prone regions (Texas, Kansas, Colorado).
How Are Mini Split Plastic Components Quality-Tested Before Shipment?
| Defect | Cause | Prevention |
|---|---|---|
| Warpage | Non-uniform cooling | Conformal cooling, balanced gates |
| Sink marks | Thick walls, low packing | Rib design, 60–80% packing pressure |
| Weld lines | Multi-gate flow fronts | Optimize gate location, raise melt temp |
| Short shot | Low injection speed | Increase speed, check venting |
| Design Rule | Target | Why |
|---|---|---|
| Wall thickness | 2.5–3.5 mm | Prevents warpage and sink marks |
| Draft angle | ≥1.5° | Clean ejection without surface damage |
| Rib-to-wall ratio | 0.5–0.6× | Stiffness without sink marks |
| Corner radius | ≥0.5 mm | Reduces stress concentration |
| Challenge | Root Cause | Solution |
|---|---|---|
| Warpage | Uneven cooling, wall thickness variation | Conformal cooling channels, uniform wall design |
| Sink marks | Excessive wall thickness, low packing pressure | Rib design, optimized packing profile |
| Color fade | UV degradation | Specify ASA or UV-stabilized compound |
| Brittle failure | Moisture absorption, low melt temperature | Pre-dry resin, verify melt temp |
Quality testing for ductless mini split plastic components follows a layered approach. Here’s how we structure our quality system:
Incoming Material Inspection: Every material lot is verified against the approved material specification before being released to production. We check melt flow index (MFI), density, color coordinates (CIELab), and moisture content. Lots outside specification are quarantined and returned to the material supplier.
First Article Inspection (FAI): The first parts off a new mold or after a significant process change are measured against the 3D nominal using a coordinate measuring machine (CMM). We check 35–50 critical dimensions on the front fascia panel alone.
In-Process Statistical Process Control (SPC): Key dimensions (snap-fit feature heights, mounting hole locations, overall flatness) are tracked on X-bar/R control charts during production. Process capability indices (Cpk) must be ≥1.33 for critical dimensions.
Finished Part Testing: Samples from each production lot are subjected to:
- Flatness / warpage measurement: Maximum 0.5 mm/300 mm for front panels
- Snap-fit engagement/disengagement force: 15–45 N engagement, <60 N disengagement
- Gloss level (60°): ±3 GU from target specification
- Color measurement: ΔE <1.5 vs. approved color master
- Izod impact strength: ≥8 kJ/m² at -20°C for outdoor parts
- Louver fatigue cycling: 100,000 open/close cycles with <2° angle deviation
| Test | Standard | Pass Criterion |
|---|---|---|
| UV weathering | ASTM D4329 | Um molde de aço P20 bem conservado para componentes de alojamento de mini-split em ABS/ASA normalmente produzirá 500.000–800.000 peças antes de necessitar de uma reconfiguração significativa. Elementos de elevado desgaste, como inserções de porta e orifícios de pinos ejetores, podem necessitar de substituição a cada 150.000–200.000 peças. A utilização de aço H13 para inserções de núcleo/cavidade em aplicações com resinas abrasivas (graus com carga de vidro) prolonga significativamente a vida útil do molde. |
| Impact resistance | ASTM D256 | No break at specified energy |
| Dimensional check | CMM / caliper | ±0.2 mm on critical dims |
| Salt spray | ASTM B117 | No corrosion after 500h |
Accelerated Weathering: Random outdoor housing samples are tested to ASTM G155 (Xenon arc) for 1,000 hours, with assessment of color shift (ΔE), gloss retention, and impact strength retained. ASA parts typically retain >85% of original impact strength at 1,000 hours; ABS drops to <60%.
What Design Innovations Are Transforming Ductless Mini Split Manufacturing?
The ductless mini split market has become intensely competitive, and OEMs are leaning on their plastic component suppliers to help differentiate product. In our production facility, we’ve been involved in several design innovation trends reshaping mini split manufacturing:
Integrated Acoustic Dampening: Rather than adding separate foam damping pads after molding, newer mini split designs integrate acoustic damping features directly into the blower housing geometry — honeycomb internal structures, constrained-layer damping ribs, and resonance-tuned chamber volumes that reduce noise by 3–5 dB without adding parts or assembly time. We work closely with acoustic engineers to validate these designs using FEA before committing to steel.
Snap-Fit Assembly Optimization: The snap-fit design4
| Housing Part | Recommended Material | Key Property |
|---|---|---|
| Outdoor unit body | ASA | UV + weather resistance |
| Indoor cassette panel | ABS/PC blend | Gloss finish, dimensional stability |
| Louvre / airflow guide | ABS or PP | Flexibility, low friction |
| Drain pan | PP | Chemical resistance |
language in mini split indoor units has evolved dramatically. Modern units can be fully disassembled for filter cleaning and maintenance without any tools in under 60 seconds, compared to 8–10 minutes for units designed a decade ago. This requires snap-fit features engineered for 500+ engagement cycles without fatigue failure.
Two-Component (2K) Molding for Soft-Touch Grips: Premium mini split models now feature overmolded TPE (thermoplastic elastomer) soft-touch grips on front panel pull-down sections, improving user experience and creating a tactile quality perception. We run these on multi-shot injection molding presses to eliminate a secondary bonding operation.
Self-Cleaning Surface Coatings: Several Japanese OEM clients have requested anti-microbial and self-cleaning nano-coatings applied in-mold (IML) or as a post-mold secondary operation. These silver ion or photocatalytic TiO₂ coatings reduce biofilm growth on the indoor unit surfaces — a meaningful selling point in post-pandemic markets.
Lightweighting Through Part Consolidation: We’ve helped clients reduce the indoor unit part count from 16 discrete injection-molded parts to 11 by redesigning with complex multi-feature single-shot parts — combining the blower housing and duct transition into a single component, for example. This reduces assembly time by 25% and eliminates potential mismatch joints.
What Are the Most Frequently Asked Questions About Ductless Mini Split Plastic Components?
What plastic is used for ductless mini split indoor unit housings?
Indoor unit housings are almost universally made from ABS (Acrylonitrile Butadiene Styrene) or ABS/PC blends. These materials offer excellent surface finish, ease of painting, and balanced stiffness/toughness at the right cost point for high-volume production. Front fascia panels typically use 2.0–2.5 mm wall thickness to balance stiffness and material cost.
Why do outdoor mini split units use ASA instead of ABS plastic?
ASA (Acrylonitrile Styrene Acrylate) has intrinsically superior UV resistance compared to ABS because its acrylic rubber phase doesn’t photodegrade under UV exposure. ABS outdoor housings typically show significant yellowing and surface chalking within 3–5 years, while ASA maintains appearance and impact strength for 10+ years. Most tier-1 mini split OEMs (Daikin, Mitsubishi, LG) specify ASA for all outdoor-facing components.
How long does injection mold tooling for mini split components last?
A well-maintained P20 steel mold for ABS/ASA mini split housing components will typically deliver 500,000–800,000 shots before requiring significant rework. High-wear features like gate inserts and ejector pin holes may need replacement every 150,000–200,000 shots. Using H13 steel for core/cavity inserts in abrasive-resin applications (glass-filled grades) extends tool life significantly.
| Quer esteja a especificar uma nova linha de produtos de mini split ou a avaliar o seu fornecedor atual de componentes plásticos, os detalhes que abordámos neste guia — seleção de materiais, diretrizes de espessura de parede, tolerâncias de encaixe por pressão, protocolos de teste UV — formam a base de um programa de componentes plásticos de qualidade que servirá bem o seu produto ao longo de toda a sua vida útil nominal. | Efficiency Level | Typical Application |
|---|---|---|
| 13–15 | Minimum efficiency | Budget residential |
| 16–20 | High efficiency | Standard residential/light commercial |
| 21–25 | Very high efficiency | Premium residential |
| 26+ | Ultra-high efficiency | Inverter premium / cold climate |
Can mini split plastic housings be recycled at end of life?
Yes, with some caveats. ABS and ASA are thermoplastics that can be mechanically recycled, but mixed plastic assemblies (ABS housing with TPE overmold, for example) require disassembly before recycling. We encourage clients to design for disassembly — using snap-fits rather than adhesive bonds — so that end-of-life units can be separated into single-material streams for recycling. Several European OEM clients now require RoHS-compliant, halogen-free plastic specifications across their entire mini split product range.
What tolerance should I specify for snap-fit features on a mini split front panel?
For snap-fit cantilever hooks in ABS operating at room temperature, we recommend a dimensional tolerance of ±0.1 mm on hook height and ±0.15 mm on deflection gap. The undercut depth should be 0.5–1.5 mm for permanent snap-fits and 0.3–0.8 mm for releasable snap-fits. Always specify the engagement and release force targets (typically 15–45 N engagement, under 60 N release) and verify through physical testing, not just calculation, as material lot variation and mold wear both affect real-world performance.
| Component | Snap-Fit Type | Assembly Benefit |
|---|---|---|
| Front panel latch | Cantilever | Tool-free removal for service |
| Filter frame | U-clip | Repeatable removal/refit |
| Drain cover | Annular | Watertight snap closure |
| Wiring duct lid | L-shaped lock | Secure one-hand closure |
What causes yellowing in mini split indoor unit plastic panels?
Indoor ABS panels yellowing is typically caused by: (1) UV exposure from sunlight through windows, (2) heat from direct sunlight on the surface over time, or (3) volatile chemical exposure (certain cleaning products, cigarette smoke, paint fumes). Standard ABS is susceptible to all three mechanisms. UV-stabilized ABS grades delay onset but don’t eliminate it. For installations in sunlit rooms, we recommend specifying ASA or UV-stabilized ABS/PC blends for the front fascia as well.
What Should You Remember About Ductless Mini Split Plastic Manufacturing?
A ductless mini split system is far more than a compressor and a fan — it’s a collection of precisely engineered injection-molded plastic components, each selected and manufactured to survive decades of mechanical stress, UV exposure, and thermal cycling.
From our position as a plastic component manufacturer, the key lessons from years of mini split production are clear: ASA for outdoor housings is non-negotiable in any serious product specification; warpage management in large flat panels requires systematic mold engineering, not trial and error; and snap-fit design is a discipline in itself, requiring fatigue life testing alongside standard dimensional checks.
The ductless mini split market’s growth means increasing competitive pressure on plastic co
| Key Takeaway | Detail |
|---|---|
| Preferred outdoor resin | ASA — 10+ yr UV stability, no painting needed |
| Wall thickness target | 2.5–3.5 mm for housing panels |
| Critical draft angle | ≥1.5° for clean ejection of large flat panels |
| Snap-fit engagement | 0.3–0.5 mm interference for ABS/ASA cantilever |
mponent quality. OEMs that partner with manufacturers who understand the full material science, processing, and quality testing chain will consistently outperform those who treat plastic housings as a commodity. We’ve seen this play out repeatedly — the brands with the most durable, visually consistent plastic components earn stronger field reputations and lower warranty return rates.
Whether you’re specifying a new mini split product line or evaluating your current plastic component supplier, the details we’ve covered in this guide — material selection, wall thickness guidelines, snap-fit tolerances, UV testing protocols — form the foundation of a quality plastic component program that will serve your product well across its full rated lifespan.
-
Peças de Plástico para Mini Split Sem Condutas: Como São Feitas: A standardized measure of cooling output divided by energy input over a typical cooling season. Higher SEER values indicate greater energy efficiency. The U.S. DOE sets minimum SEER2 ratings for residential systems: 13.4 (North) and 14.3 (South) as of 2023. ↩
-
ASA (Acrylonitrile Styrene Acrylate): A weatherable engineering thermoplastic structurally similar to ABS but with an acrylic rubber phase replacing the polybutadiene rubber, providing inherent UV stability and outdoor weathering resistance without relying solely on UV-stabilizer additives. Widely specified for outdoor HVAC housings. ↩
-
Injection molding: A high-volume plastic manufacturing process in which molten thermoplastic resin is injected under pressure into a precision steel mold cavity, held until solidified, and ejected as a finished part. The dominant process for producing complex plastic components with tight tolerances at scale. See the injection molding process guide ↩
-
Snap-fit assembly: A design approach using cantilevered or annular plastic hooks that deflect during engagement and return to their original geometry when the mating feature is fully seated, creating a permanent or semi-permanent mechanical connection without fasteners. Critical for tool-free serviceability in mini split indoor units. ↩





