20+ Years OEM/ODM Experience
+86 152 2111 0591
🇫🇷

HVAC Industry Solutions

空気配分ブログ | カスタムHVACソリューション | HVACore

Latest Blog

Stay updated with the latest trends, innovations, and insights from the HVAC manufacturing industry.

Read More
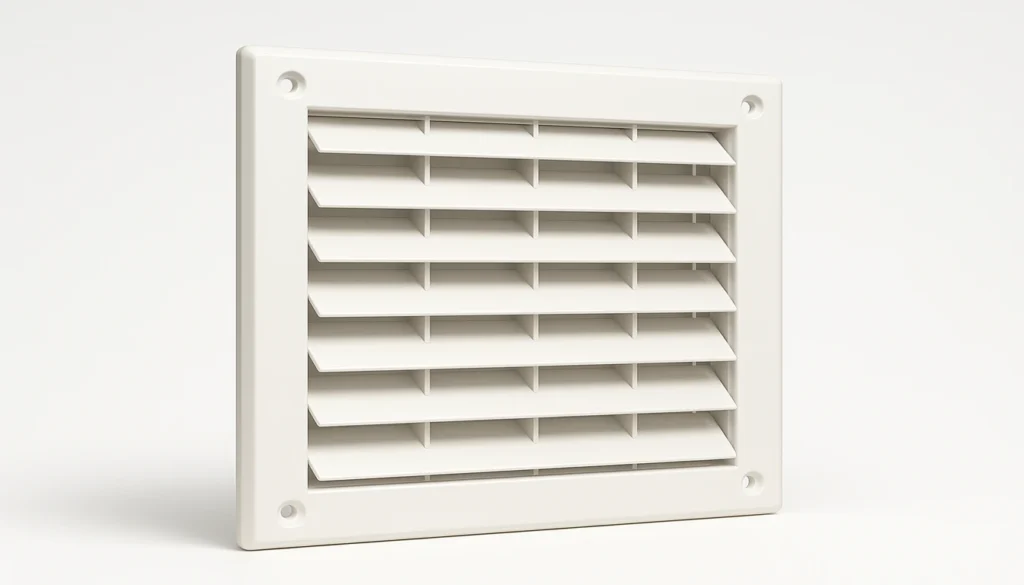
Injection molded air vent grille for HVAC
HVACore定風量プラスチック部品製造サマリー

グリルエリアのP20鋼をベリリウム銅(BeCu)に置き換えました。BeCuは鋼よりも3~4倍速く熱を伝導し、内部のウォーターラインなしで「ブレード」が熱をメインモールドベースに放散できるようにします。

Key Takeaways An open area ratio of 50–65% balances airflow performance with mold steel durability; exceeding 70% risks blade fracture within 10,000 cycles. Steel blade thickness must match air slot width; slots narrower than 3 mm leave steel blades that cannot be internally water-cooled and overheat. Knit lines in grille ribs retain only 60–80% of base material strength — managing them through gate placement is mandatory. Shut-off surfaces require 3–7° draft angle to prevent galling and flash as the mold accumulates wear. Beryllium copper inserts in blade areas reduce mold temperature by 15–20°C, cutting cycle time by up to 25%. What Is the Core Trade-Off in Molded Grille Design? The […]
Read More
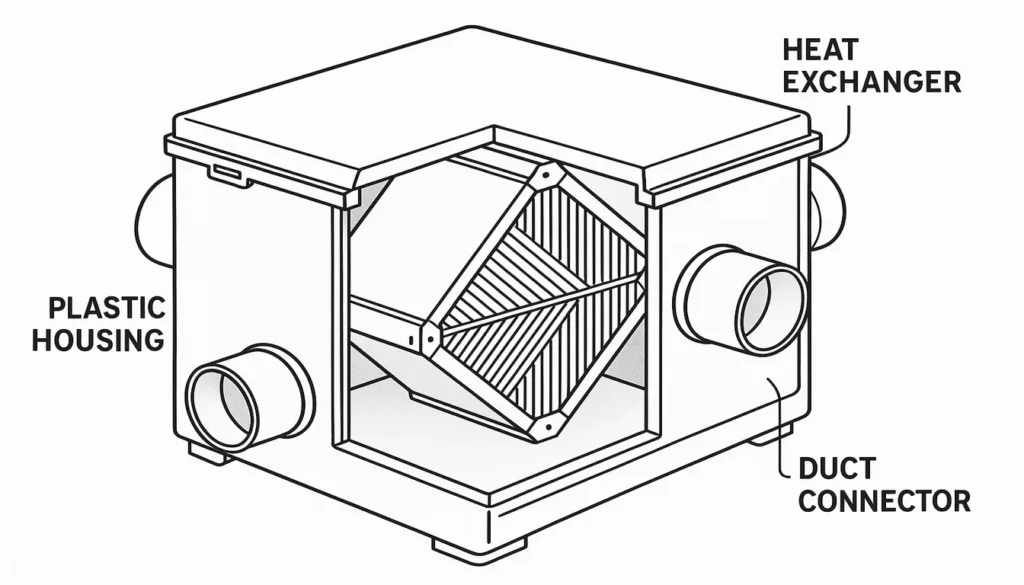
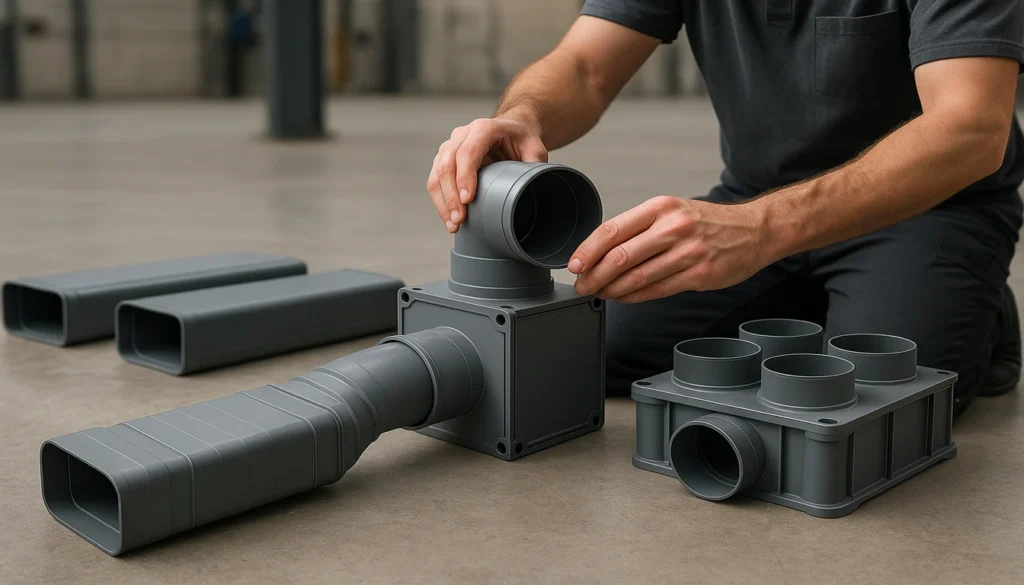
Read More
HRV Plastic Components: Materials, Design & Manufacturing
3月 21, 2026

主要ポイント HRVプラスチック部品—筐体パネル、コアフレーム、ドレンパン、ダクト接続部—はシステムの効率、耐久性、および組立速度を直接決定します。

HRVプラスチック部品:材料、設計、製造
Read More
Read More
Injection molding HVAC duct assembly installation
3月 20, 2026

射出成形HVACダクトアセンブリ取り付け

キーポイント 射出成形はスナップフィットとインターロック部品設計により、HVACダクトワークの設置工数を最大40%削減します。精密射出成形は±0.1mmの寸法公差を実現し、漏れのないダクト継ぎ手を保証することでシステム効率を15~25%向上させます。射出成形による熱可塑性ダクト部品は80~120℃の連続使用温度に耐え、腐食や湿気に強い特性を持ちます。モジュラー式射出成形ダクトシステムは材料ロスを30%削減し、板金加工では不可能な複雑な形状を実現します。射出成形は大量生産されるHVAC部品において一貫した品質を提供し、初回合格率は95%を超えます。なぜ射出成形部品がHVACダクトワーク設計を変えつつあるのか?射出成形は暖房、換気、[…]のダクトワーク設計を根本的に変革しています。
Read More
Read More
キーポイント 射出成形では、HVACダンパーブレード、アクチュエーターハウジング、ピボットブラケットを0.1mm以下の公差で製造します。熱可塑性材料...
3月 19, 2026

キーポイント 射出成形では、HVACダンパーブレード、アクチュエーターハウジング、ピボットブラケットを0.1mm以下の公差で製造します。熱可塑性材料...

主なポイント 射出成形では、HVACダンパーブレード、アクチュエータハウジング、ピボットブラケットを0.1mm未満の公差で製造します。ABS、POM、ガラス充填ナイロンなどの熱可塑性材料は、耐食性と40-60%の軽量化において金属製ダンパー部品を上回ります。適切に設計された射出成形ダンパー部品は、500Paの差圧で1%未満の気密漏れ率を達成します。標準ダンパーブレードのサイクルタイムは1個あたり15~35秒で、大量生産が可能です。ゲート位置と冷却チャネル設計は、ダンパーアセンブリの寸法安定性において最も重要な2つの要素です。HVACダンパー部品に射出成形が選ばれる理由は?射出成形1がHVAC2ダンパー部品製造を支配している理由は、[…]
Read More
Read More
主なポイント ABS(アクリロニトリル・ブタジエン・スチレン)は、耐衝撃性、寸法安定性、表面仕上げ品質の最適な組み合わせを提供し…
3月 18, 2026

主なポイント ABS(アクリロニトリル・ブタジエン・スチレン)は、耐衝撃性、寸法安定性、表面仕上げ品質の最適な組み合わせを提供し…

キーポイント 多色射出成形は、単一の金型キャビティ内で2つ以上の樹脂流を1回の連続サイクル中に結合し、色分けされたHVACコンポーネントにおける成形後の組み立て、接着、塗装工程を不要にします。シーケンシャル二色成形(第1射+第2射)がHVAC用途で主流であり、構造用樹脂を基調色とし、視覚的ガイドやシール要素として二次弾性体や対照色を組み合わせることが可能です。多色部品のサイクルタイムは単一材料品より5~15%長くなりますが、人件費と組み立てコストの削減により通常は金型の複雑さを相殺し、部品総コストを30~50%低減します。多色射出成形の金型設計には、回転プラテン、同期コア動作、[…]が必要です。
Read More
Read More
キーポイント マルチカラー射出成形は、一連の連続サイクル中に単一の金型キャビティ内で二つ以上の樹脂流を組み合わせる技術であり、...
3月 17, 2026

キーポイント マルチカラー射出成形は、一連の連続サイクル中に単一の金型キャビティ内で二つ以上の樹脂流を組み合わせる技術であり、...

Key Takeaways Multi-color injection molding combines two or more resin flows within a single mold cavity during one continuous cycle, eliminating post-molding assembly, gluing, or painting operations for color-differentiated HVAC components. Sequential two-shot molding (first shot + second shot) dominates HVAC applications, enabling a primary structural resin in one color paired with a secondary elastomer or contrast color for visual guidance or seal elements. Cycle time for multi-color parts runs 5 to 15 percent longer than single-material equivalents, but labor and assembly cost reductions typically offset tooling complexity, resulting in 30 to 50 percent lower total component cost. Mold design for multi-color injection molding requires rotating platens, synchronized core movements, […]
Read More
Chat on WhatsApp